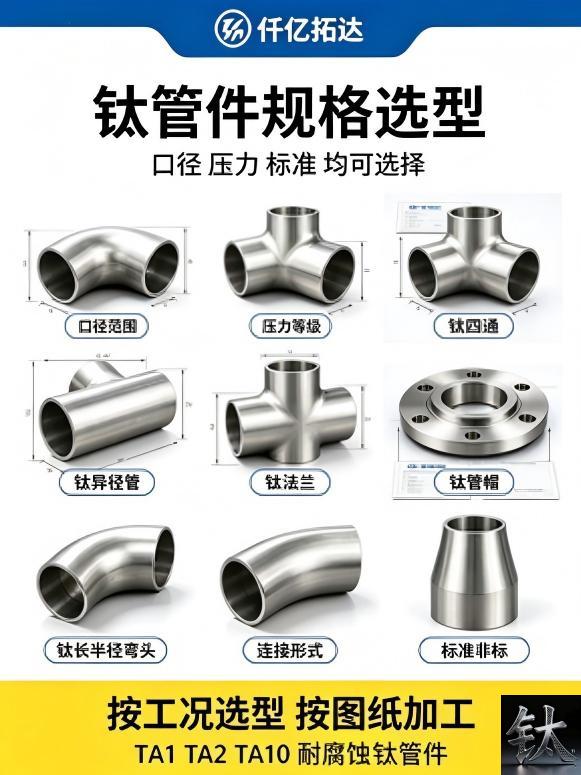
Titanium Elbows, Tees and Reducers: The Full-Range Bevel and Fit-Up Dimension Chain
| Спецификация | Nominal size: elbow, tee and reducer combinations across the published DN and schedule matrix under ASTM B363 |
|---|---|
| Применимый стандарт | Mating part: adjoining pipe OD and measured wall, butt weld bevel, branch saddle opening and the flange or equipment nozzle |
| Состояние материала | Governing drawing: piping isometric revision, ASTM B363 edition named in the PO and the ASME B16.9 or MSS SP-43 edition for dimensions |
| Контроль и упаковка | Tolerance basis: centre to end envelope, bend radius, concentric or eccentric offset, bevel angle and root face, wall transition and local minimum thickness |
Описание продукции: Full range means a size matrix, not a stock promise. Radius, concentric or eccentric orientation, schedule transition and bevel pairing decide fit-up.
Обзор продукции
Titanium Elbows, Tees and Reducers: The Full-Range Bevel and Fit-Up Dimension Chain
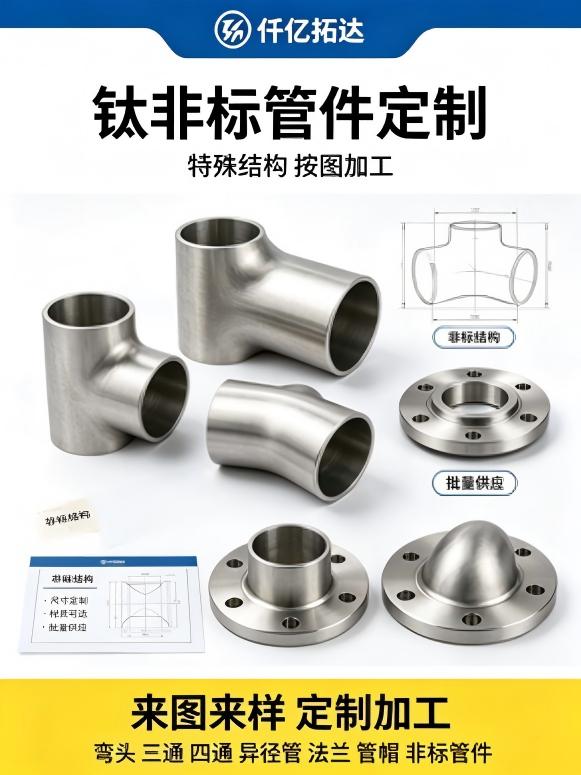
A full range of titanium elbows, tees and reducers is a size matrix, not a stock promise: a 1.5D elbow and a 3D elbow of the same nominal size differ in centre to end dimension, a concentric and an eccentric reducer share the same end sizes but not the same centre line, and a fitting cut to nominal schedule leaves an internal step when the adjoining pipe wall minimum differs. Three interfaces therefore decide the joint before any welding starts: the bevel to the pipe, the branch opening to the run pipe, and the wall transition across a schedule change. Our fittings selection decision tree, our what B363 hides guide and our fitting receiving wall inspection guide settle which fitting to buy and what the product standard covers; this article starts where they stop, at the bevel, the branch opening and the wall transition.
At a Glance: Eight Decisions Between a Size Matrix and a Weldable Joint
| Item | What the decision turns on |
|---|---|
| The short answer | Full range describes a matrix of size, radius and schedule combinations, not a promise that any one combination sits on a shelf ready to weld |
| The governing identity | Fit-up clearance equals the available envelope minus the fitting centre to end dimension, minus the bevel land and root gap, minus the OD and wall mismatch at the joint |
| The radius trap | A 1.5D and a 3D elbow of the same nominal size occupy different space, so a spool cut for one does not accept the other |
| The orientation trap | A concentric and an eccentric reducer have the same end sizes but different centre lines, and on a horizontal run the flat side direction is a drawing decision |
| The schedule trap | A fitting bevel cut to nominal schedule leaves an internal step when the adjoining pipe wall minimum differs |
| The thinning trap | Intrados wall reduction is a forming result, and a thickness measured at one point does not describe the thinnest section at the bevel |
| The branch trap | A tee branch opening must be cut to the measured run OD and kept clear of the run longitudinal seam, with reinforcement set by the drawing |
| The one document | A 14-Line Full-Range Fitting Bevel and Fit-Up Verification Sheet: check, basis, method, criterion, who signs |
Rows three and five hide most of the rework, and our elbow tee size judgment guide plus our B363 elbow tee and reducer stock page give the product context. A stockholder can certify a heat number and a nominal size; it cannot certify the fit-up clearance at your spool without measuring the centre to end dimension, the bevel land and the adjoining pipe wall on that joint. Read the rest of this article as the second check line that starts where the certificate stops.
The All-in-the-Range Trap: Full Means a Size Matrix, Not a Stock Promise
A catalogue that says full range is describing a matrix: nominal size crossed with bend radius, with schedule, with concentric or eccentric form and with equal or reducing branch. Each cell of that matrix has its own centre to end dimension, its own bevel preparation and its own local wall minimum. Our fittings selection decision tree and our elbow tee and reducer page already cover how to choose the cell; this article uses that choice as a known input rather than restating the decision path.
Availability is a separate question from fit. A stockholder can hold many combinations, but a specific radius in a specific schedule in a specific grade may still be a made-to-order item, and a made-to-order fitting arrives with its own dimensional record. Confirm the exact combination on the purchase order, the named dimensional standard edition and the delivery condition before the spool is cut.
Full range is a buying statement. Centre to end, bevel land and wall minimum are the fit-up dimensions of one delivered fitting.
The trap closes when a fabricator issues one bevel preparation sheet for an entire order spanning several sizes and schedules. Confirm the dimensional standard edition, the radius, the schedule and the concentric or eccentric form for each item, then measure the delivered centre to end and bevel rather than the nominal value. Our ASTM B363 fittings page and our B363 fittings guide give the standard baseline.
Where the Space Goes: 1.5D and 3D Elbows and the Envelope Chain
The fit-up clearance is one identity, not a tolerance. It equals the available envelope on the isometric, minus the measured centre to end dimension of the fitting, minus the bevel land and root gap at each end, minus the OD and wall mismatch at the joint. Bend radius enters that chain directly: a long radius elbow commonly quoted as 1.5D and a 3D elbow occupy different centre to end lengths for the same nominal size, so swapping one for the other moves both weld stations and can collide with a support, a nozzle or an adjacent line.
Measure the centre to end on the delivered fitting, not from the table. Forming tolerances, end trimming and bevel preparation all change the as-delivered dimension, and a small difference at a large nominal size becomes a large gap at the second weld. Check both ends, because an elbow is not necessarily square at both faces.
Wall at the bend is the third term. Forming thins the extrados and thickens the intrados, so the wall minimum at the bevel is not the nominal wall and not the wall measured at the crown. Published thinning figures disagree between product standards, forming notes and buyer guides, so we publish the conflict rather than one value.
The Orientation Nobody Checks: Concentric Versus Eccentric on a Horizontal Run
A concentric and an eccentric reducer share the same two end sizes, so a purchase order that names only the sizes leaves the centre line undefined. On a horizontal run that choice is a drainage and venting decision: an eccentric reducer installed with the flat side up keeps the top of the line level and avoids a pocket, while the opposite orientation traps gas or liquid at the crown. The direction is a drawing decision, not a fitter preference.
Geometry follows the orientation. An eccentric reducer offsets one centre line, so the adjoining pipe on that side sits at a different elevation and the support, the branch opening and the next fitting all move with it. Substituting a concentric reducer to resolve a fit problem changes the elevation of the whole run.
Two reducers can share end sizes and still not share a centre line. Mark the flat side before the joint is tacked.
The branch opening is the third orientation decision. A tee requires a saddle cut on the run pipe sized to the measured run OD, kept clear of the run longitudinal seam, and reinforced according to the branch detail. A template built from nominal OD leaves a gap that no weld passes.
Three Fit-Up Interfaces: Bevel to Bevel, Branch Opening, and Wall Transition
Bevel to bevel and the root gap
The fitting bevel and the pipe bevel must share an included angle, a root face and a land that produce the root gap in the qualified WPS. A fitting delivered with a standard bevel and a pipe cut to a different angle meet at a drifting gap around the circumference. Check both bevels with an angle gauge at mapped stations and machine the transition from measured dimensions. Our WPS qualification guide and our GTAW shielding guide cover the joint record and the root discipline; the WPS revision decides the angle and the land.
The branch opening and the reinforcement
The branch saddle is cut to the measured run OD and to the branch OD, not to a nominal template. Where the branch approaches the run diameter the opening removes a large part of the run wall, so the reinforcement detail and the weld sequence matter as much as the cut profile. Confirm the cut profile, the seam clearance and the reinforcement pad or set-on detail against the isometric revision.
The schedule transition and the internal step
Where a fitting schedule differs from the adjoining pipe schedule, the joint needs a transition bevel machined from the measured wall minimum on both sides, not from the nominal schedule. An external taper that looks smooth can leave a sharp internal step that disturbs flow and concentrates stress. Measure wall at mapped stations around both ends and machine the transition accordingly.
When the Published Centre to End and Bevel Numbers Disagree: Publish the Conflict, Not One Value
Ask several sources for a centre to end tolerance, a bevel angle, a permitted wall thinning at the intrados or a branch reinforcement rule and you get a spread, not one table. Dimensional standards, product standards, fabrication codes and our own pages use different nominal sizes, schedules and measuring bases. Presenting any one figure as the correct value would be false precision.
| Quantity | Figures in conflict | Why they disagree | What to confirm |
|---|---|---|---|
| Centre to end dimension tolerance | One dimensional standard quotes a fixed plus and minus band per nominal size; another scales it with size; a project specification adds a tighter spool fit allowance | Different editions, nominal sizes and whether the bevel is included in the dimension | ASME B16.9 or MSS SP-43 edition, measured centre to end at both ends and the isometric envelope |
| Intrados wall thinning after forming | One forming note quotes a percentage of nominal wall; a product standard sets a minimum wall at any point; a buyer page quotes no thinning figure | Different forming routes, bend radii and definitions of local minimum | Named product standard edition, mapped ultrasonic survey and the acceptance clause |
| Bevel angle and root face | One WPS quotes a fixed included angle; another scales it with wall thickness; a fitting supplier ships a standard bevel with a stated land tolerance | Different schedules, welding processes and root gap targets | Qualified WPS revision, angle gauge reading and a mapped land survey on both parts |
| Long radius versus short radius designation | Guides commonly quote 1.5D for long radius and 1D for short radius; a project may specify 3D for a special bend; some tables omit the designation entirely | Different dimensional standards and custom bend requirements | Purchase order radius, measured centre to end and the isometric envelope |
| Eccentric reducer offset | Dimensional tables give the offset for some sizes and not others; a layout guide quotes a flat side rule without a number; a buyer page lists no offset | Different nominal size pairs and whether the offset is to the centre line or to the flat side | Isometric elevation, measured offset and the marked flat side |
| Branch reinforcement requirement | One code uses an area replacement rule; a project specification names a pad thickness; a light duty guide requires no calculation below a size ratio | Different design codes, pressures and branch to run diameter ratios | Design code edition, branch detail on the isometric and who reviews the calculation |
Our ASTM B363 fittings page and our fittings selection decision tree show why the edition and the chosen matrix cell must be named, and our EN 10204 3.1 certificate page shows the form of a traceable record. A chart is a buying aid; the measured centre to end, the bevel survey and the signed verification sheet are the tie breakers. Chapter ten gives six actions that settle the numbers.
Two Independent Check Lines: Fit-Up Here, Selection and Receipt There
Which elbow, tee or reducer to buy, what ASTM B363 covers, and whether the received fitting meets its wall minimum are selection, specification and receipt questions, not fit-up questions. They belong to the line that our fittings selection decision tree, our what B363 hides guide and our fitting receiving wall inspection guide already cover. We do not restate that line here.
Keep the two records separate. The selection and receipt file holds the purchase order, the mill certificate, the named standard edition, the radius and schedule combination and the receiving wall survey. The fit-up file holds the piping isometric revision, the measured centre to end, the concentric or eccentric orientation, the bevel and land survey on both parts, the wall minimum map, the branch saddle profile and seam clearance, the root gap and the signed 14-line sheet.
Limitations and Failure Conditions: Eight Full-Range Fitting Fit-Up Rejection Triggers
[Geometry] Trigger 1 - Spool cut to a catalogue centre to end dimension instead of the delivered fitting
Recalculate the fit-up clearance from the chain: available envelope minus measured centre to end, minus the bevel land and root gap, minus the OD and wall mismatch. A layout built from a table omits the forming and bevel result. Judge against the approved calculation and the piping isometric revision.
[Geometry] Trigger 2 - Short radius and long radius elbows swapped without re-checking the envelope
Name the radius on the purchase order and measure centre to end on the delivered fitting, then confirm the envelope, the support positions and the adjacent lines on the isometric. A 1.5D and a 3D elbow of one nominal size do not occupy the same space. Our elbow radius page gives the radius context.
[Geometry] Trigger 3 - Intrados wall minimum ignored because one crown reading passed
Map wall thickness around the bend and at both bevels, then check the local minimum against the named product standard edition and acceptance clause. Forming thins the extrados and thickens the intrados, so one reading cannot describe the joint. Our what B363 hides guide covers the forming result.
[Fit] Trigger 4 - Concentric reducer substituted for an eccentric one, or flat side installed without a drawing instruction
Confirm the concentric or eccentric form and the flat side direction against the piping isometric revision and the line list, then measure the delivered offset. Two reducers can share end sizes and still not share a centre line. Our tee and reducer guide gives the application context.
[Fit] Trigger 5 - Fitting bevel and pipe bevel prepared to different angles or root faces
Check both bevels with an angle gauge at mapped stations around the circumference, then machine the transition from measured dimensions to produce the root gap in the qualified WPS. A drifting gap around a large joint cannot be closed by welding technique. Our GTAW shielding guide covers the root discipline. In a dispute, re-machine the bevel and re-measure the gap.
[Fit] Trigger 6 - Schedule transition machined from nominal wall leaving an internal step
Measure wall at mapped stations on both the fitting end and the adjoining pipe, then machine the transition from the measured minima on both sides. A smooth external taper can hide a sharp internal step. Our butt weld fittings cut to spec page gives the preparation context.
[Process] Trigger 7 - Branch saddle cut from a nominal OD template and crossing the run longitudinal seam
Cut the saddle to the measured run OD and branch OD, mark the run seam angle and confirm the clearance and the reinforcement detail against the piping isometric revision. A nominal template leaves a gap that no weld closes. Our ASTM B363 fittings page gives the product context.
[Process] Trigger 8 - No bevel survey, no wall minimum map, no signed verification sheet or lost heat-to-fitting traceability
Reconcile every delivered fitting, cut spool and welded joint against the heat number, the piping isometric revision, the orientation mark and the signed sheet. A fitting whose centre to end and bevel survey cannot be rebuilt is a reject regardless of a clean mill certificate. Our fitting receiving wall guide shows what the receipt record proves.
The 14-Line Full-Range Fitting Bevel and Fit-Up Verification Sheet
| # | Fit-up check | Basis drawing or standard edition | Measurement method | Acceptance criterion | Who signs |
|---|---|---|---|---|---|
| 1 | Standard edition, grade, nominal size and schedule named | Purchase order and MTC | Document review | One designation with revision | Buyer QA |
| 2 | Exact matrix cell confirmed: radius, form and schedule | Purchase order and isometric revision | Document review and item mark check | One confirmed combination per item | Piping engineer |
| 3 | Dimensional standard edition named for centre to end | ASME B16.9 or MSS SP-43 edition in the PO | Document review | One edition, no mixed tables | Piping engineer |
| 4 | Centre to end measured at both ends of the fitting | Measurement plan and drawing revision | Calibrated height gauge or tape at both faces | Both values logged, envelope checked | Fabrication inspector |
| 5 | Concentric or eccentric form and flat side direction marked | Piping isometric revision and line list | Orientation mark review on the fitting | Flat side matches drawing, offset logged | Fabrication inspector |
| 6 | Wall minimum mapped around the bend and at both bevels | Named product standard edition | Ultrasonic survey at mapped stations | Local minimum logged, inside criterion | Fabrication inspector |
| 7 | Adjoining pipe OD and wall minimum measured | MTC and measurement plan | OD grid and ultrasonic wall survey | Mismatch carried into the chain | Fabrication inspector |
| 8 | Bevel angle, root face and land checked on both parts | Qualified WPS revision and joint detail | Angle gauge and feeler around the circumference | Uniform bevel, land inside criterion | Welding inspector |
| 9 | Schedule transition machined from measured minima | Machining plan and WPS | Wall survey after machining | No internal step above criterion | Fabrication supervisor |
| 10 | Branch saddle profile cut to measured run OD | Piping isometric revision and branch detail | Template check against measured OD | Profile fits, gap inside criterion | Fabrication inspector |
| 11 | Run seam clearance from branch opening confirmed | Isometric revision and seam record | Layout check on the marked run | No intersection, clearance logged | Piping engineer |
| 12 | Branch reinforcement detail and calculation reviewed | Design code edition and branch detail | Calculation review | Reinforcement accepted per named code | Design engineer |
| 13 | Root gap and high-low measured at fit-up | WPS acceptance clause | Internal gauge at mapped stations | Gap and step inside criterion | Welding inspector |
| 14 | Cumulative envelope fit and signed verification sheet | General arrangement and dimension chain | Measure offset at fit-up and reconcile records | Offset inside criterion, hold released | Quality lead and buyer |
Line four is often answered with a catalogue centre to end value instead of a measurement at both ends, line six with one crown reading instead of a mapped wall survey, line nine with a nominal schedule instead of measured minima and line ten with a nominal OD template. Our fittings selection decision tree and our fitting receiving wall guide separate selection and receipt evidence from fit-up work. Our WPS qualification guide shows the form of a signed joint record, and our equipment leak repair guide shows the downstream cost of an undocumented joint.
Six Verification Actions When Centre to End and Bevel Figures Conflict
- Require every acceptance value to carry its document, revision and clause. Name the ASTM B363 edition, the ASME B16.9 or MSS SP-43 edition, the piping isometric revision and the qualified WPS before quoting any centre to end or bevel band. Our B363 fittings guide is a product reference, not the governing clause.
- State the sample condition and measuring method: as delivered, bevelled or re-cut, and the centre to end dimension measured at both ends rather than the nominal table value. Our B363 fitting stock page gives the buying baseline.
- Publish the fit-up chain before cutting any spool: available envelope, measured centre to end, bevel land and root gap, OD and wall mismatch, and the branch saddle profile. A calculation is a prediction; the measured root gap at fit-up is the record. Our butt weld fittings cut to spec page covers end preparation.
- Name who reviews the conflict: buyer quality, piping engineer, fabrication supervisor and welding inspector, with authority to accept or hold. Our WPS qualification guide shows that qualification is a signed decision.
- Keep records independent with their own dates: purchase order and MTC, receiving wall survey, centre to end measurement, orientation and flat side mark, bevel and land survey, wall minimum map, branch saddle profile and the signed verification sheet. Our EN 10204 3.1 certificate page covers what the mill record proves.
- Use trigger-based re-verification: any radius or schedule change, concentric to eccentric substitution, re-cut, re-bevelling, seam re-marking or opened hold forces reassessment. Our equipment leak repair guide and our equipment layup guide show the downstream cost.
Most of these cost nothing at planning and a great deal after a spool is cut and a joint is ground out. Ask for the purchase order clause, the measured centre to end, the bevel survey, the branch saddle profile and the signed verification sheet for the same fitting. We are a stockholder, not the author of your piping isometric; where figures come from published guides we label them, and where they disagree we give the disagreement and the action.
Summary: Choose a Nominal-Range Layout if, Choose a Re-Measured Fit-Up Chain if
Choose X if: a nominal-range layout with a signed verification sheet
- The purchase order names the standard edition, the radius, the schedule and the concentric or eccentric form, and the piping isometric revision states the envelope and the flat side direction.
- The delivered centre to end is measured at both ends and the fit-up chain uses the bevel land, the root gap and the OD and wall mismatch.
- The branch saddle is cut to the measured run OD, kept clear of the run longitudinal seam and matched to the reinforcement detail.
- The bevel angle, root face, wall minimum map, root gap and the 14-line sheet are signed per line before release.
Escalate to a fit-up hold or an isometric review if:
- A clean mill certificate or a clean receiving wall survey is the only fit-up evidence offered; our receiving wall guide is an earlier gate, not this one.
- The word full range was treated as a geometry guarantee and no radius or schedule combination was confirmed per item.
- Published centre to end, thinning or bevel figures disagree and no one has named the governing dimensional standard edition.
- A concentric reducer was substituted for an eccentric one, or the flat side was installed without a drawing instruction.
- The bevel survey, the wall minimum map, the branch saddle profile or a signed verification sheet is missing.
Choose Y if: a re-measured fit-up chain and a new spool cut
- The radius, schedule or concentric form was substituted; settle the dimension chain again before cutting. Our small batch fittings page covers the non-standard combinations that make this common.
- The design controls a branch reinforcement or a flat side elevation, so a wall mismatch cannot be absorbed. Our process equipment buyers guide gives the equipment context.
- The buyer cannot produce a centre to end measurement, a bevel survey or a signed verification sheet; set up the fabrication records first.
- Which fitting to buy is still in dispute; keep that on the selection line and read our fittings selection decision tree while the fit-up line stays independent.
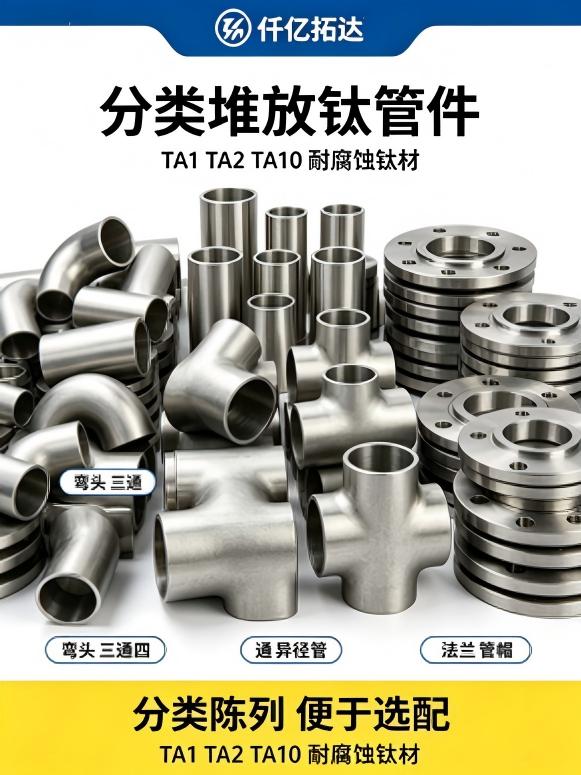
The whole subject reduces to one sentence: a nominal size is not a joint, because the size matrix tells you what to order while the tolerance chain tells you whether the delivered fitting will close the spool. When you enquire, send the nominal size and schedule, the bend radius, the concentric or eccentric form, the standard edition, the piping isometric revision and the measured pipe OD and wall. We are a Baoji China Titanium Valley titanium stockholder with roughly 800 tonnes in stock, including a wide matrix of elbows, tees and reducers; we cut to non-standard and small-batch sizes, work from customer drawings, read and certify to ASTM, ASME and GB standards, export-pack in house, and dispatch confirmed in-stock orders the same day. Send us the piping isometric and the fitting list, and we will tell you what we can ship and which decisions belong with your team. Request a quote
Frequently Asked Questions
Does a full range of elbows, tees and reducers mean every combination is ready to weld?
A full range describes a size matrix, not a stock promise. Each cell of that matrix has its own centre to end dimension, bevel preparation and local wall minimum, and a specific radius in a specific schedule and grade may be a made-to-order item. A spool cut for a short radius elbow does not accept a long radius elbow, and a support set for one centre line does not hold the other.
Can a short radius elbow be swapped for a long radius elbow of the same nominal size?
A swap changes the geometry. A long radius elbow commonly quoted as 1.5D and a 3D elbow have different centre to end lengths, so both weld stations move and the fitting can collide with a support, a nozzle or an adjacent line. Measure centre to end on the delivered fitting at both ends and re-check the envelope, the support positions and the adjacent lines against the piping isometric revision.
Why does the flat side of an eccentric reducer need a drawing instruction?
Because a concentric and an eccentric reducer share the same end sizes but not the same centre line. On a horizontal run the flat side direction is a drainage and venting decision: installed flat side up it keeps the top of the line level and avoids a pocket, while the opposite orientation traps gas or liquid. It also offsets the adjoining pipe elevation, which moves supports and branch openings.
How much wall thinning at a bend is acceptable before the bevel is machined?
There is no single published value that governs. One forming note quotes thinning as a percentage of nominal wall, a product standard sets a minimum wall at any point, and a buyer page quotes no thinning figure. The figures disagree because forming routes, bend radii and definitions of local minimum differ.
Must the transition bevel be re-machined when the fitting and pipe schedules differ?
A schedule change does not by itself force rework, but the bevel must be machined from the measured wall minima on both sides rather than from the nominal schedule. A smooth external taper can hide a sharp internal step that disturbs flow and concentrates stress. Measure wall at mapped stations around both ends, machine the transition from those readings and verify the internal profile.
Who signs the centre to end measurement and the bevel survey?
The fabrication inspector signs the centre to end measurement at both ends against the measurement plan and the piping isometric revision, and the welding inspector signs the bevel angle, root face and land survey against the qualified WPS. A catalogue dimension is not a measurement, and one bevel reading is not a survey because the gap drifts around a large circumference. Published centre to end tolerances disagree, so name the governing dimensional standard edition and confirm the measured values.
Is the fit-up check the same as the fitting selection decision or the receiving wall inspection?
They are independent check lines at different gates. The selection line decides which elbow, tee or reducer to buy, using the decision tree, the purchase order, the named standard edition and the grade. The receiving line checks the delivered wall minimum and certificate.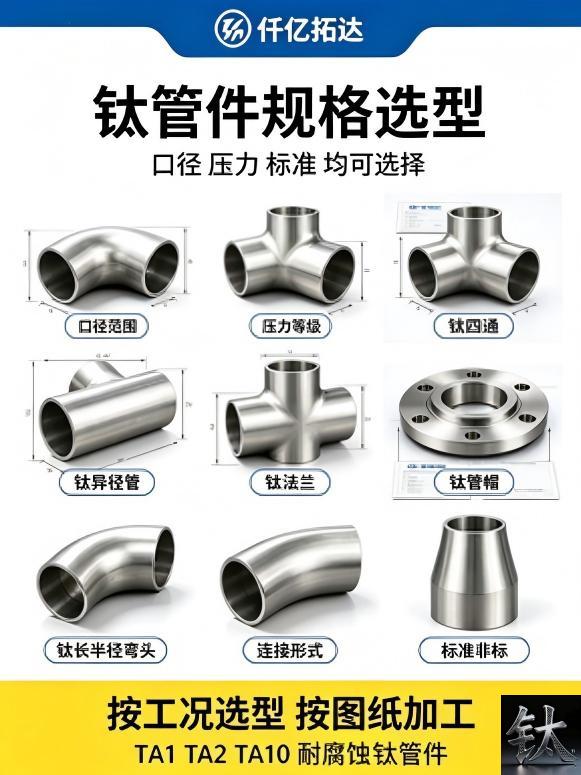
Request a Quote for Titanium, Nickel or Zirconium
Tell us what you need. Send the points below and we reply with live stock status, price and lead time — usually the same day.
Send us these 6 points (or just attach your drawing / old supplier spec)
| 1 | Material grade — Gr2 / Gr5 / Gr7 / Gr12, Ni200 / Ni201 / Monel 400, Zr702… |
| 2 | Form — plate / tube / bar / wire / fitting / flange / fastener / equipment |
| 3 | Size & tolerance — thickness×width×length / OD×WT / diameter |
| 4 | Quantity — kg / pcs / m (small batch and non-standard sizes welcome) |
| 5 | Standard — ASTM B265 / B338 / B348, ASME B16.5, EN 1092-1… |
| 6 | Application & destination — helps us pick the right grade and certifications |
Not sure how to fill this? Send your drawing or an old supplier's specification sheet — we will break it down for you.
Reach us directly
Email: [email protected]
WhatsApp / WeChat:+8618829679311 leave your number on the form
Or use the inquiry form on this page — attach your drawing and we will respond within one business day.
Why buyers come to us
Stock holder in Baoji Titanium Valley with ~800 t inventory · cut-to-size and small batch · drawing-based machining for non-standard parts · we read ASTM / ASME / GB specs · export experience · same-day response on quotes.
Опишите ваши требования — марка, размер и количество. Ответим в течение 24 часов.
Предпочитаете чат? WhatsApp +86 188 2967 9311 или напишите на [email protected].
- Titanium Price Today (9 Nov 2026): Plate, Tube, Rod & Wire
- Что такое титан фланец| ASME B16.5 ASTM B381 Gr2 Gr5 титановые флажк
- ASME B16.5 титановая флажка класса 2 DN100-DN600 Класс 150/300 FOB
- Gr2 Titanium Sheet Price FOB Shanghai | ASTM B265 In Stock
- Titanium Price Today (26 октября 2026 г.): отчет о рынке Китая
Контактное лицо: Wang Xiaoning
Телефон: +86-917-355-7966
Эл. почта: [email protected]
WhatsApp: +86 188 2967 9311
Компания: Shaanxi Qianyi Tuoda Technology Co., Ltd
Адрес: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China