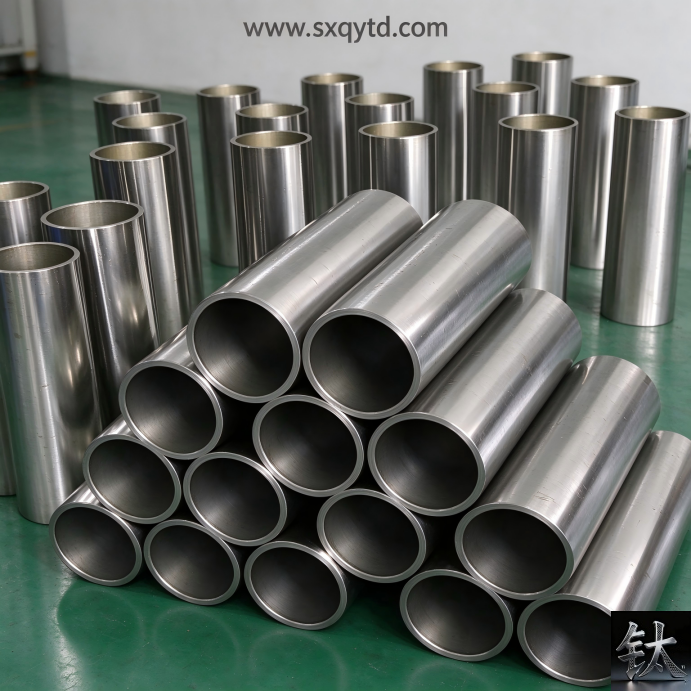
Welded vs Seamless Titanium Tube Selection Guide \| B338/B861/B862, Real Procurement Logic
| Specification | welded vs seamless titanium tube selection guide, ASTM B338 welded titanium tube, ASTM B861 seamless titanium pipe, titanium tube weld joint efficiency ASME, when to use seamless titanium tube, welded |
|---|
Product Description: Welded vs seamless titanium tube — not which is better, but which fits the spec. B338/B861/B862 boundaries, weld annealing + ECT, pressure/fatigue/U-bend decision tree, Gr2 vs Gr9 logic. Copy-paste en
Product Overview
Welded vs Seamless Titanium Tube Selection Guide | Not "Better", Just "Right"
Meta Description: Welded vs seamless titanium tube — not which is better, but which fits the spec. B338/B861/B862 boundaries, weld annealing + ECT, pressure/fatigue/U-bend decision tree, Gr2 vs Gr9 logic. Copy-paste enquiry template.
Overview — The Wrong Choice Costs More Than the Premium
Buyers ask "welded or seamless?" as if one is superior. It isn't. A properly made welded Gr2 B338 tube, vacuum-annealed with 100% eddy current testing, outruns a badly specified seamless tube in a condenser bundle every day of the week. The real question is: what does your datasheet, medium, and pressure class actually force?
This guide is written for EPC procurement, heat-exchanger designers, and maintenance buyers who've seen a PO rejected by third-party inspection because "B338 welded" was quietly swapped for "B861 seamless" — or vice versa.
First, Kill the Terminology Mix-Up
| Term | Measured by | Standard family | Job |
|---|---|---|---|
| Tube | OD × Wall | ASTM B338 (seamless + welded) | Heat transfer, exchanger bundle, precision fit |
| Pipe | NPS × Schedule | B861 (seamless only) / B862 (welded) | Pressure transport, process line |
If the BOM says "tube" but quotes B861, something's off. B861 has no weld seam and no welded version — that's B862's lane.
How Each Is Made (Why It Matters)
Welded Titanium Tube (B338 / B862)
Strip/sheet (B265) → roll form → TIG weld → vacuum anneal → ECT/UT → cut.
Post-weld anneal recrystallizes the HAZ; modern weld is not a "weak line" in seawater/chemical service when NDT is done right.
- Wall thickness very uniform → better heat transfer, easier tube-sheet expansion
- Long lengths, large OD, thin wall = cost winner
- 100% ECT on weld is the non-negotiable, not a bonus
Seamless Titanium Tube (B338 seamless / B861)
Billet (B348) → pierce → roll → cold pilger/draw → anneal → NDT.
No longitudinal seam, continuous grain flow.
- No HAZ, no weld joint efficiency factor to discount
- Fatigue/vibration/cyclic pressure → structural margin
- Small OD, high wall, aerospace/medical/high-pressure gas
- Costs more, longer lead, size range tighter on big OD
Standard Boundary (Don't Cross Without QA Sign-Off)
| Standard | Form | Covers | Key test emphasis |
|---|---|---|---|
| ASTM B338 | Seamless + Welded | HX / condenser / evaporator tube | ECT, flattening, flaring, hydro |
| ASTM B861 | Seamless ONLY | Pressure pipe, process transport | UT, hydro, tensile |
| ASTM B862 | Welded ONLY | Large-Dia welded pipe | Weld NDT, anneal, hydro |
Rule of thumb: heat transfer → B338; pressure transport → B861 (seamless) or B862 (welded). Forcing B861 into a tubesheet bundle is over-spec; forcing welded into a code U-tube without flattening/flaring proof is a rejection waiting to happen.
Decision Tree — 5 Questions, in Order
- Does the drawing say "seamless only"? → Stop. Seamless B338 or B861. No debate.
- Is it a U-tube or code-stamped HX (ASME/PED)? → B338 seamless (ductility verification for bending/expansion). Welded needs explicit buyer acceptance + flattening/flaring on weld.
- Pressure / fatigue? → Gas >10 MPa, pulsating hydraulic, aerospace → seamless. Liquid low-mid pressure → welded OK with joint-efficiency calc.
- Diameter & length? → OD >400mm or km-scale condenser runs → welded is economically unavoidable.
- Budget vs risk? → Welded saves 20–40% on large bundles; seamless buys margin where failure isn't an option.
Weld Seam Weak Point — The Honest Answer
Old fear: "weld = corrosion start." Modern reality:
- Full argon shield TIG → no oxidation in seam
- Vacuum anneal → HAZ microstructure ≈ base metal
- 100% ECT + hydrostatic → pinhole/leak screened out
- ASME BPVC weld joint efficiency factor still applies — engineer must use η in pressure calc
So: welded is NOT "second class". It's "code-class only if NDT + anneal + joint efficiency are on the PO". We write those into the quote, not into marketing.
Gr2 vs Gr9 Across the Two Processes
| Grade | Welded fit | Seamless fit |
|---|---|---|
| Gr2 / TA2 | Excellent — desalination, HX, chemical | Available, often over-spec unless pressure demands |
| Gr9 (Ti-3Al-2.5V) | Rare — weld + anneal doable, but aerospace specs usually mandate seamless | Default for hydraulic/aerospace |
If the spec says Gr9, assume seamless unless engineering signs off otherwise.
Testing Matrix (Write This Into the PO)
| Test | Welded B338 | Seamless B338 | B861 pipe |
|---|---|---|---|
| Eddy Current (ECT) | 100% weld + body | Per PO | UT替代/补充 |
| Hydrostatic | Yes (per PO pressure) | Yes | Core test |
| Flattening | Yes (weld at specified angle) | Yes | Per PO |
| Flaring | Yes | Yes | Per PO |
| UT | Wall/thickness check | Per PO | Standard for thick wall |
| MTC | EN 10204 3.1 (3.2 on request) | 3.1 default | 3.1 default |
Cost & Lead Reality (No Bluff)
| Type | Relative cost | Lead (ex-works) |
|---|---|---|
| B338 welded Gr2 | Baseline | Shortest (stock cut same-day) |
| B338 seamless Gr2 | +15–30% | Medium |
| B861 seamless Gr2 | +25–45% vs welded tube | Longer (pilger schedule) |
| Gr9 seamless | Premium | Heat-confirm |
Cost difference is real; over-specifying seamless on a 5km condenser bundle can blow the budget with zero reliability gain.
Typical Industry Defaults
- Condenser / MSF-MED HX: B338 welded Gr2 — industry mainstream
- U-tube HX, code-stamped: B338 seamless Gr2
- Seawater process pipe SCH10S: B861 seamless or B862 welded (spec-dependent)
- Aerospace hydraulic: B861 Gr9 seamless, AMS-controlled
- HPLC/capillary: seamless only (no seam, no dead volume)
- Architectural/structural: welded, cost-driven
Procurement Red Flags (QA Reject List)
- PO says B338 but cert arrives as B861 → heat/standard mismatch
- "MTC available" but no heat number on tube tag
- Welded tube with no ECT report referenced
- Flattening/flaring omitted on B338 welded
- 3.1 passed as 3.2 without TPI signature
- Gr9 quoted as welded without engineering waiver
Enquiry Template (Copy-Paste)
Application: HX / condenser / process pipe / hydraulic / R&D ___
Standard required: ASTM B338 / B861 / B862 ___
Form: welded / seamless / "either if NDT ok"
Grade: Gr2 / Gr9 / other ___
Size: OD×wall ___ mm  OR  NPS___ SCH___
Length: ___ m × ___ pcs
Pressure: design ___ MPa, medium ___, temp ___°C, cyclic? Y/N
Bend: U-tube? radius ___ / straight only
NDT: ECT 100% / UT / hydro ___ MPa / flatten+flare
Cert: EN 10204 3.1 / 3.2 (TPI: ___)
Budget driver: cost-first / code-first
FAQ — Welded vs Seamless Titanium Tube
Q1: Is welded titanium tube "lower quality"?
A: No. Properly annealed + 100% ECT welded B338 is standard in global desalination/HX. "Lower quality" only describes welded tube WITHOUT post-weld anneal or NDT — which we don't supply.
Q2: Can welded replace seamless in a heat exchanger?
A: In straight, low-pressure, non-code HX — yes, with buyer acceptance. In U-tube or ASME-code bundles — no, unless flattening/flaring + ductility are proven and QA signs off.
Q3: Why does seamless cost more?
A: Billet pierce + cold pilger + draw is labor/energy heavy; yield loss higher. You pay for grain continuity and no joint-efficiency discount.
Q4: Does ASME require seamless?
A: Not universally. Welded is allowable with joint efficiency factor η in BPVC. But client spec or U-tube bending often de facto forces seamless.
Q5: Gr2 welded vs Gr2 seamless — same corrosion resistance?
A: Chemically identical grade. Corrosion behavior in flowing seawater is equivalent when weld is annealed. Crevice/stagnant still drives Gr7, not weld method.
Q6: How do I prove the weld isn't a leak risk?
A: ECT report (full length) + hydrostatic at 1.5× design + flattening/flaring on sample. Ask for NDT scope in writing.
Q7: Big OD (>12") — can it be seamless?
A: Technically yes but economically painful. B862 welded is the sane choice for large-Dia low-mid pressure.
Q8: MTC for welded — 3.1 enough?
A: For most projects yes — mill authorized inspection rep, heat-matched. 3.2 only when TPI witness mandated in PO (cannot be retro-added).
Q9: Aerospace — ever welded Gr9?
A: Rare; only with spec waiver + full post-weld heat treat + NDT. Default = seamless.
Q10: Which do YOU stock?
A: Gr2 B338 welded + B861 seamless rotate in stock; B338 seamless on heat-confirm; Gr9 seamless project-drawn. We don't pretend all grades sit on shelf.
Request a Quote / Get a Spec Check
Email: sales@[yourdomain].com
Send the enquiry block above. We reply within 24h: confirm welded/seamless fit, live heat, NDT scope, EXW/FOB quote — and tell you if your PO is over-specified before you overspend.
About: Baoji Titanium Valley inventory holder. Welded B338 + seamless B861/B338 Gr2 on rotation, Gr9 seamless on heat-confirm. We don't push seamless to inflate the quote — we match the standard to the failure mode. Tag = MTC = crate; NDT scope written before cutting, not after.
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China