Titanium Flange Procurement Guide: Grades, Standards, Inspection and Acceptance
Titanium Flanges are simple parts with a long list of ways to get them wrong. The failures that matter almost never come from the material itself — they come from a grade mixed up with another grade, a standard from the wrong system, or a technical detail nobody wrote into the contract.
This guide covers what a buyer actually has to specify: three grades, three standard systems, five details that get omitted, four procurement traps and an acceptance procedure.
1. The Three Grades You Will Actually Be Quoted
Most titanium flange enquiries resolve to one of three grades. The differences in strength, corrosion behaviour and price are large enough that a mix-up cannot be corrected later by machining or by a gasket change.
| Property | TA2 — Commercially Pure | TA10 — Ti-0.3Mo-0.8Ni | TC4 — Ti-6Al-4V |
|---|---|---|---|
| UNS number | R50400 | R53400 | R56400 |
| ASTM grade | Grade 2 | Grade 12 | Grade 5 |
| Tensile strength | ≥ 345 MPa | ≥ 485 MPa | ≥ 895 MPa |
| Yield strength | ≥ 275 MPa | ≥ 345 MPa | ≥ 825 MPa |
| Composition | Ti ≥ 99.0% | Ti + 0.3% Mo + 0.8% Ni | Ti-6Al-4V |
| Suited to | Sea water, chlorides, organic acids, general chemical | Dilute sulphuric acid, reducing media, crevice-prone joints | High mechanical load, high pressure, structural joints |
| Relative price | 1.0× | 1.3 – 1.5× | 2.5 – 3.0× |
How to verify which one you received. The mill test certificate is the starting point — check the UNS number and the chemistry, not just the grade name printed on the cover. Beyond the certificate, a spectrometer check on a sample from the delivered lot takes minutes and settles the question definitively.
Colour is not a reliable check. TA2, TA10 and TC4 are all silver-grey; TA10 is marginally darker and TC4 marginally lighter, but the difference is not something to base an acceptance decision on, and lighting changes it. Price is a weaker check still — it tells you what someone believed they were selling, not what they shipped.
One point worth stating plainly: TC4 is not a premium version of TA2. It is stronger and considerably less corrosion resistant in many chemical media, and it is harder to weld. Specify TC4 when the problem is mechanical load, not when the problem is corrosion.
2. The Three Standard Systems
Standard systems are not interchangeable. They differ in dimension units, in pressure class designation and in the physical geometry of the joint. Mixing them produces flanges that do not bolt to the mating flange on the other side of the line — the single most expensive procurement error because it is only discovered at installation.
| System | Standard | Sizes | Pressure Designation | Used For |
|---|---|---|---|---|
| Chinese national | GB/T 9112 (dimensions); GB/T 21225 (Titanium Flanges) | DN15 – DN600, metric | PN10 / PN16 / PN25 / PN40 | Domestic general industrial piping |
| Chinese chemical industry | HG/T 20592 | DN15 – DN600, metric | PN-designated | Chemical pressure piping, corrosive service |
| American | ASME B16.5 | NPS ½" – 24", imperial | Class 150 / 300 / 600 | Export projects, international specifications |
| European | EN 1092-1 | DN10 – DN2000, metric | PN-designated | European projects |
Where the systems actually diverge. The pressure designations look convertible and are not. Class 150 and PN16 are routinely treated as equivalent, and they are close, but the bolt circle and bolt hole diameter differ — an ASME Class 150 flange and an EN 1092-1 PN16 flange of the same nominal size will not reliably bolt together. On a DN150 pair, the bolt circles differ by roughly 10 mm.
Everything you need to check is normally marked on the flange rim: standard number, grade, DN or NPS, pressure class and facing code. If those markings are absent or incomplete, that alone is grounds to hold the goods.
3. Five Details Buyers Leave Off the Contract
These five items cause more installation failures than wrong material does, because their absence is invisible until the joint is assembled.
3.1 Surface roughness on the sealing face
For a standard raised face, specify Ra 3.2 – 6.3 μm. This is the commercial-machining range that seals reliably with a spiral wound or sheet gasket and is what a properly finished RF face delivers.
Finer finishes are available and sometimes required — Ra 1.6 μm or better for confined facings such as male/female and tongue and groove, and Ra 0.4 – 0.8 μm for ring joint grooves. Specify these when the facing calls for them, and expect a price difference, because they require additional machining passes and inspection.
What you must not do is write only "RF" and leave roughness undefined. Suppliers will default to whatever their tooling produces, and coarse-tooled faces are a leading cause of weeping joints that pass a hydrostatic test cold and leak at operating temperature.
3.2 Weld neck thickness
For a WN flange, the neck wall thickness must be at least the pipe wall thickness plus 1 mm, per HG/T 20592 and ASME B16.5. This is not a nominal requirement — the neck has to carry the same load as the pipe, and an under-thickness neck becomes the weak point in the spool.
Write the minimum neck thickness into the technical annex. Where the schedule is stated only as a pipe schedule (SCH 40, SCH 80), confirm what wall thickness that resolves to in the actual diameter, because the same schedule number means a different wall at different sizes.
3.3 Bolt hole count
Bolt hole count is fixed by size and standard, and it must match the mating flange exactly.
| Metric (GB / HG) | Bolts | Imperial (ASME B16.5) | Bolts |
|---|---|---|---|
| DN15 – DN50 | 4 | NPS ½" – 1" | 4 |
| DN65 – DN150 | 8 | NPS 1¼" – 2½" | 8 |
| DN200 – DN300 | 12 | NPS 3" – 12" | 8 to 12, varies by class |
The imperial column is where mistakes happen: above NPS 2½", bolt count depends on pressure class as well as size, so the count cannot be read from the diameter alone. Check the specific table for the class you are ordering.
3.4 Facing type
RF — raised face — is the general-purpose default for conventional service. MFM — male and female — is used for medium and high pressure chemical duty where the gasket needs confinement. RJ — ring joint — is for very high pressure and severe duty.
State the facing code and the machining accuracy together. "RF" alone specifies the geometry but not the surface, and the surface is what seals.
3.5 Marking and packing
A conforming titanium flange carries, on the rim: standard number, grade, DN or NPS, pressure class, facing code, manufacturer mark and heat or batch number. Incomplete marking is a legitimate reason to reject, because it breaks traceability back to the mill certificate.
Packing matters more than it appears. Flange faces are finish-machined surfaces; a wooden case with foam separation and stretch wrapping protects the sealing faces from impact and from each other. Flanges shipped loose in a crate arrive with dinged faces, and a dinged face is a leak path that no gasket will seal.
4. Four Procurement Traps
A price well below the market. Titanium is a commodity with a traceable input cost, so a quotation significantly under the prevailing level is not a bargain — it is a signal. The saving is usually recovered through grade substitution, reduced machining tolerance, or omitted testing. Counter it in the contract: full mill test certification and UT on a defined sampling basis, with the lot number traceable to the delivered goods.
A delivery date that compresses the process. Standard lead time for non-stock Titanium Flanges is measured in weeks, not days. When a date is demanded that does not allow for material, machining and inspection in sequence, something in that sequence gets shortened — and it is never the machining. Build the delivery date and the inspection scope into the contract together, so that shortening one is visibly a breach of the other.
Specifying size and pressure only. "DN100 PN16" does not specify a flange. It leaves the standard system, the facing, the roughness, the neck thickness and the bolt pattern all open. Put all of them in the technical annex: DN, PN or Class, standard system, facing code, Ra value, neck thickness and material standard with grade.
Inadequate packing for shipment. Damage in transit is discovered at installation, by which time the schedule is already lost. Specify the packing method and the condition on arrival as part of the order, not as an afterthought.
5. Procurement Procedure, Five Steps
- Define the duty. Medium, concentration, temperature, pressure, and how often the joint will be opened. The last one is routinely forgotten and determines whether a confined gasket is needed.
- Select the grade against the medium. Sea water and chlorides — TA10 (or TA2 in clean flowing sea water). Dilute sulphuric acid — TA10. Concentrated sulphuric acid at ambient — TA2. Organic acids — TA2. Reducing acids — TA9. Fluoride-bearing media — not titanium at all.
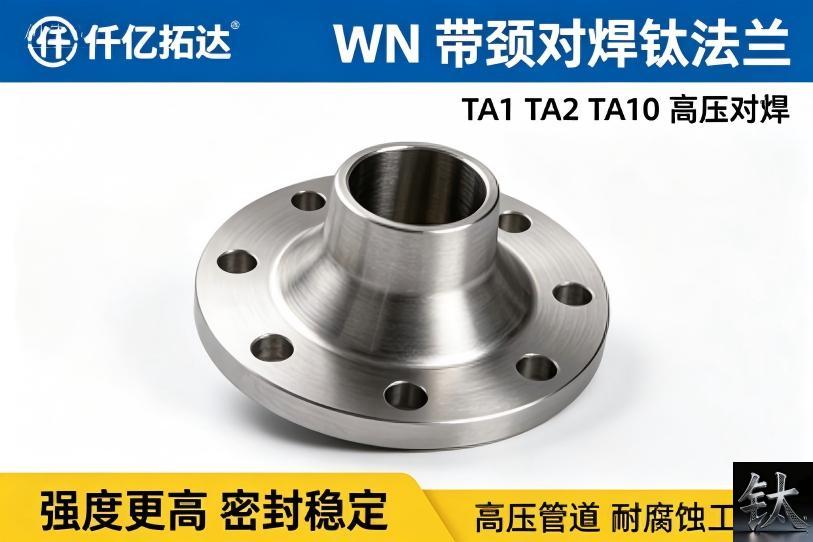
- Fix the structure and the standard system. PL for ambient low pressure, SO for general medium pressure, WN for high temperature with thermal cycling, IF for extreme duty. Then pick one standard system and stay in it for the whole spool.
- Write the five details into the technical annex. Facing code with Ra value, minimum neck thickness, bolt hole count and diameter, facing machining accuracy, marking requirements.
- Set acceptance before the order, not after. Mill test certificate with traceable lot number, third-party composition and mechanical reports, PT on sealing faces for critical duty, UT or RT on a defined sampling rate, and the packing specification.
6. Acceptance Checklist
| Check | Method | Pass Condition |
|---|---|---|
| Grade | Spectrometer on delivered lot | Chemistry matches specified UNS number |
| Documentation | Certificate review | MTC lot number traceable to goods; third-party report present |
| Marking | Visual on rim | Standard, grade, size, class, facing, heat number all present |
| Dimensions | Bolt circle, hole diameter, face-to-face | Within standard tolerance; bolts to mating flange |
| Sealing face | PT and roughness gauge | No indications; Ra within specified range |
| Internal soundness | UT or RT on sample basis | No shrinkage cavity, inclusion or lamination |
| Packing | Open and inspect | Faces undamaged; separation present; no transit bruising |
We hold Titanium Flanges in TA1, TA2, TA9, TA10 and TC4 across PL, SO, WN and IF structures, in ASME B16.5, EN 1092-1, JIS B2220 and HG/T 20592 configurations — stock items dispatched within 7 days, non-standard sizes to drawing typically within 15 days. Send us the duty, the standard system and the facing code and we will come back with a complete specification including grade, roughness, neck thickness and inspection scope.
Email: sales@sxqytd.com | WhatsApp: +86 188 2967 9311
- 12 октября 2026 г. Спотовый рынок титановых материалов | Актуальные
- Отчёт по ценам на титан — 29 сентября 2026 г. | Цены на плиты, трубы
- Технология обработки и стандарты контроля качества титановых мешалок
- Основные конструкции титановых мешалок и рекомендации по выбору
- Преимущества титановых мешалок при высоких температурах и сильной ко
Контактное лицо: Wang Xiaoning
Телефон: +86-917-355-7966
Эл. почта: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Компания: Shaanxi Qianyi Tuoda Technology Co., Ltd
Адрес: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China