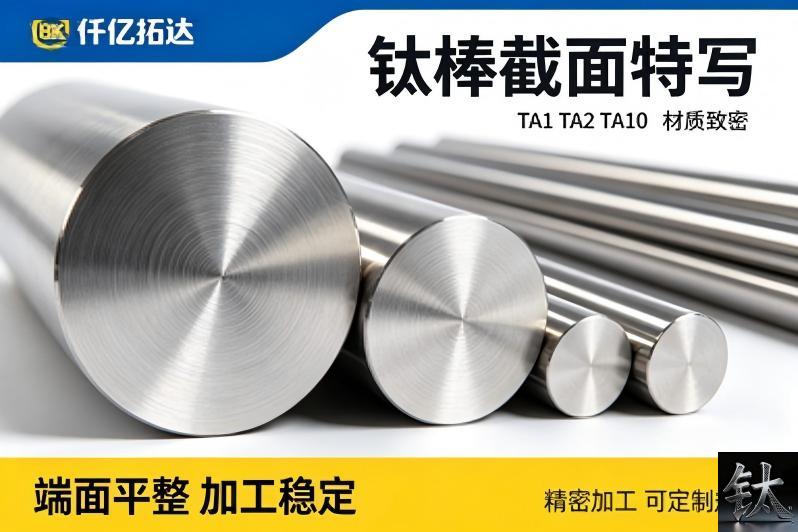
Titanium Forged Bar for Flange Making \| Gr2/Gr5 (TC4) Flange Billet, ASTM B348/B381 Route, UT-Ready
| Specification | titanium forged bar for flange making, titanium flange billet Gr2 Gr5 TC4, ASTM B348 forged bar B381 flange, titanium forged round bar flange blank Baoji, forged Ti-6Al-4V flange stock, titanium disc |
|---|---|
| Reference Price | $10.00 – $50.00 |
Product Description: Titanium forged bar for flange making from Baoji — Gr2/TA2 & Gr5(TC4) flange billet, open-die forged, annealed, UT per PO, EN 10204 3.1 heat-traceable. B348供坯 + B381最终锻件双路径。Quote with flange drawing &
Product Overview
Titanium Forged Bar for Flange Making | Gr2 / Gr5 (TC4) Flange Billet, UT-Ready
Meta Description: Titanium forged bar for flange making from Baoji — Gr2/TA2 & Gr5(TC4) flange billet, open-die forged, annealed, UT per PO, EN 10204 3.1 heat-traceable. B348 billet + B381 finished forging dual route. Quote with flange drawing & class.
Overview — A Flange Is Only as Sound as Its Billet
A flange is not "a shape turned on a lathe" — it is "density delivered by forging". Using a plain hot-rolled bar to machine a large flange carries internal risk: eccentricity, directional porosity, retained scale, and UT rejection. Forged bar (open-die forged bloom/bar) goes through upsetting and drawing-out cycles — grains are refined, flow lines align radially along the flange profile. That is the billet a high-pressure, seawater, or acid-service flange actually needs.
We supply flange billets: forged round bar, forged disc, and forged ring — selected by application. Billet supply follows ASTM B348 (forged/annealed bar stock); finished flange forgings are accepted to ASTM B381 (F-2/F-5, etc.). Two separate lines — your PO must name which one.
Forged Bar vs Rolled Bar for Flange Blank
| Factor | Hot-Rolled Bar Blank | Forged Bar Blank (This Page) |
|---|---|---|
| Internal soundness | Moderate; strong directionality | Upset-forged, porosity healed, uniform |
| Grain structure | Elongated along rolling direction | Equiaxed; transverse/longitudinal balanced |
| UT pass rate | Risky on large sections | Far more reliable on large diameters |
| Scale / eccentricity | Heavy peel allowance needed | Controlled forge + peel stock |
| Cost | Lower | Higher (forging ratio + heats built in) |
| Application | Low-pressure, non-critical, static | PN16+, seawater, acid, ASME B16.5 flanges |
One-line rule for procurement: small-bore low-pressure flanges — rolled bar is fine. DN80+, PN40+, sour/hydrogen/sea/FGD service — go forged bar or forged disc.
Three Billet Forms — How to Choose
| Form | Best for | Note |
|---|---|---|
| Forged round bar | WN flange necks, small-to-mid DN integral flanges | Φ80–300mm routine; larger = forged disc |
| Forged disc / bloom | Slip-on plates, large DN integral flanges, tube-sheet hybrids | OD calculated from flange OD + machining allowance |
| Forged ring (rolled ring) | Large-DN WN, blind flanges, lap joints | Material-saving; grain flow follows ring direction, good fatigue |
Stock Scope (Honest)
| Grade | Form | Size | Condition | Status |
|---|---|---|---|---|
| Gr2 / TA2 (R50400) | Forged bar / disc / ring | Bar Φ80–350mm; disc Φ200–1200mm project | As-forged / annealed (M) | Common bar sizes rotating; disc/ring to drawing |
| Gr5 / TC4 (R56400) | Forged bar / disc | Bar Φ80–300mm; larger on project | Annealed; STA on PO | Common sizes on hand |
| Gr7 / Gr12 | Forged bar | Per drawing | Annealed | Heat-confirm |
| Gr23 ELI | Forged bar / disc | Project | ELI + F136 chain | Separate PO |
Honest note: flange forgings are not "every size on a click-buy shelf". DN / PN / facing (RF/FF/RTJ) dictates billet diameter and allowance. Send the drawing first; we quote forging ratio and heats.
Chemistry (ASTM B348 / B381 Ref.)
| Element | Gr2 / F-2 | Gr5 / F-5 (TC4) |
|---|---|---|
| Ti | Balance | Balance |
| Fe max | 0.30% | 0.40% |
| O max | 0.25% | 0.20% |
| N max | 0.03% | 0.05% |
| H max | 0.015% | 0.015% |
| C max | 0.08% | 0.08% |
| Al / V | — | 5.5–6.75 / 3.5–4.5% |
Mechanical Floor (Annealed, Reference)
| Grade | UTS min | YS min | Elong | RA |
|---|---|---|---|---|
| Gr2 / F-2 | 345 MPa | 275 MPa | ≥20% | ≥30% |
| Gr5 / F-5 | 895 MPa | 828 MPa | ≥10% | ≥25% |
Values reference ASTM B348 / B381 annealed minima. Final flange forging acceptance = B381 F-2/F-5 + current edition + PO matrix.
UT & Forging Acceptance (Write Into PO)
- 100% volumetric UT on billet (ASTM E2375 / B381 NDE direction), FBH calibre per PO grade
- Surface PT per B381 forging surface inspection; repair welding prohibited on forgings per spec
- Forging ratio recorded on MTC; heat count / finish-forge temp available on process sheet
- EN 10204 3.1 (mill-authorized IR); 3.2 (SGS/BV/TÜV) witness PO-fronted, not back-signed
- Grain size / beta fleck / alpha-case testing added per sour-service / aero PO
- Heat traceability: ingot → forged billet → finished flange, one heat one cert
Machining Allowance (Align With Your Shop)
| Item | Typical allowance |
|---|---|
| OD turning | 3–6mm per side (by DN and billet dia.) |
| Thickness | 4–8mm per face (larger DN = larger value) |
| WN neck bar | OD leave + end facing stock |
| Facing | RF/RTJ finish-machined in-house; forging blank does NOT pre-form seal groove |
| Straightness / flatness | Checked after stress-relief anneal |
Allowance is not "the bigger the safer" — more allowance = heavier forging = higher unit price. Give us DN + PN + standard (ASME B16.5 / HG / EN1092), we back-calculate the minimum economic billet.
Grade Selection by Flange Service
| Service | Recommend | Reason |
|---|---|---|
| Seawater / Cl⁻ / hypochlorite | Gr2; Gr7 for aggressive reducing acid | Corrosion-first; Gr2 sufficient for PN med-low |
| Hot brine / acid media | Gr7 / Gr12 | Pd / Mo-Ni crevice resistance |
| High-pressure PN40+ / aero / power | Gr5 TC4 | Strength-to-weight; thinner flange profile |
| Implant / medical (non-pipe) | Gr23 ELI + F136 chain | Separate cert lineage |
Flange Standard Alignment
- Billet supply: ASTM B348 (forged bar) / GB/T 2965 (domestic TC4 forged bar route)
- Finished forging: ASTM B381 F-2 / F-5 / F-7 / F-12
- Dimensions: ASME B16.5 / B16.47 / EN1092 / HG/T20592 / JIS B2220 / DIN
- Pressure class: Class 150–2500 / PN6–PN100+ (per drawing)
- Facing: RF / FF / RTJ / MFM / TG
Enquiry Template (Copy-Paste for Flange Buyers)
Flange standard: ASME B16.5 / EN1092 / HG/T20592 ___
DN / NPS: ___   PN / Class: ___
Type: WN / SO / BL / PL / RTJ flange ___
Grade: Gr2 / Gr5(TC4) / Gr7 / Gr23 ___
Blank form: forged round bar / disc / ring ___
Billet dia (if bar): Φ___ mm
Disc OD × Thk: ___ × ___ mm
Ring OD × ID × H: ___ × ___ × ___ mm
Condition: as-forged / annealed (M) / STA
UT: B381 level / E2375 FBH ___ / 100% volumetric Y/N
Surface: descaled / pickled / peeled / rough-turned
Cert: EN 10204 3.1 / 3.2 (TPI: ___)
Machining: rough forged only / finish-machined flange?
Qty: ___ pcs   Target port: ___
FAQ — Titanium Forged Bar for Flange Making
Q1: Can B348 forged bar be delivered as a finished flange?
A: No — don't mix them. B348 is the billet material standard; finished flange forgings are accepted to ASTM B381 (F-2/F-5). We issue B348 + MTC for billet supply; the forging house issues B381 forging cert against the finished part. State clearly in PO.
Q2: At what DN should I switch from bar to disc/ring?
A: Rule of thumb — DN80–100 starts the conversation at higher pressure; DN150+ high-pressure or seawater almost always goes disc or ring. Bar-turned large flanges work but scrap and UT risk rarely justify it.
Q3: How much more does forged bar cost vs rolled?
A: You pay for forging ratio + heats + UT-ready soundness. Small DN low-pressure = rolled saves money. High-pressure / sour service = forged pays back the day the flange doesn't fail.
Q4: Can you guarantee zero defects?
A: No honest supplier does. We run 100% volumetric UT + surface PT per PO grade. Contract language: "accepted per B381, FBH calibre ___, reject on non-conformance." Honesty beats marketing.
Q5: Can Gr5 flanges be welded?
A: Yes — GTAW with pure argon backing, post-weld anneal recommended. STA-condition flanges require re-heat-treat review before welding; don't weld aged stock without evaluation.
Q6: Do you pre-form RTJ grooves in the forging?
A: No. Forging blank leaves finish-machining stock; RTJ/RR grooves are precision-machined by the shop to drawing. Hardness and groove geometry stay in-spec.
Q7: Is repair welding allowed on flange forgings?
A: B381 prohibits unauthorized repair welding on forgings. Surface indications are removed by grinding + UT re-check; beyond limits = reject. Write this into incoming inspection SOP.
Q8: Straightness / flatness of forged billets?
A: Checked after stress-relief anneal. Large discs are controlled by thickness variation / flatness — don't apply bar straightness tolerances to disc blanks.
Q9: Dispatch lead time?
A: Common forged bar sizes on hand → same-week dispatch after PO. Large disc/ring to-drawing → lead quoted honest per ingot + forge schedule. No pretending from a shelf that isn't there.
Q10: Sample / test coupon?
A: Same-heat test block (mechanical / UT reference) supplied with batch. Full-size trial forging quoted as separate project.
Request a Quote
Email: sales@[yourdomain].com
Send flange standard + DN/PN + type + grade + blank form (bar/disc/ring). Reply within 24h: forging-ratio proposal, billet sizing, UT grade, MTC type, dispatch date.
About: Baoji Titanium Valley billet supplier. Titanium forged bar for flange making — Gr2/TA2 & Gr5(TC4) open-die forged bar/disc/ring, annealed, UT per PO, EN 10204 3.1 heat-traceable. B348 billet supply and B381 finished forging acceptance kept on separate lines — no passing rolled bar as forging. Calculate the billet before the quote.
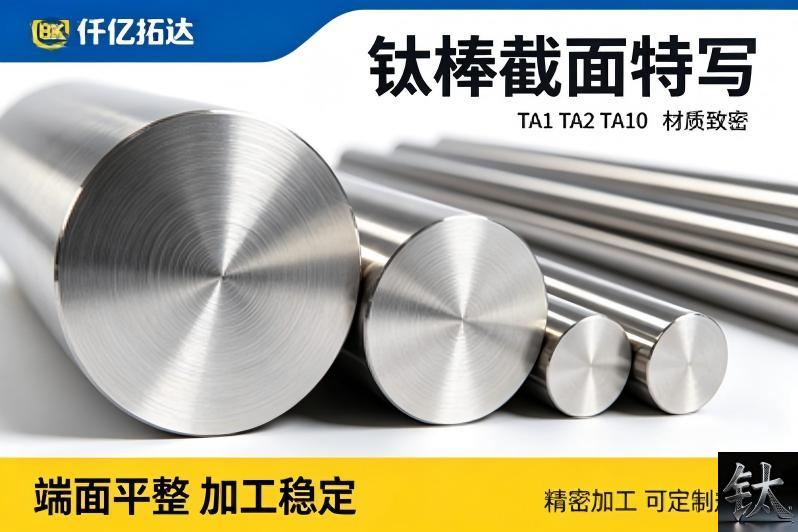
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China