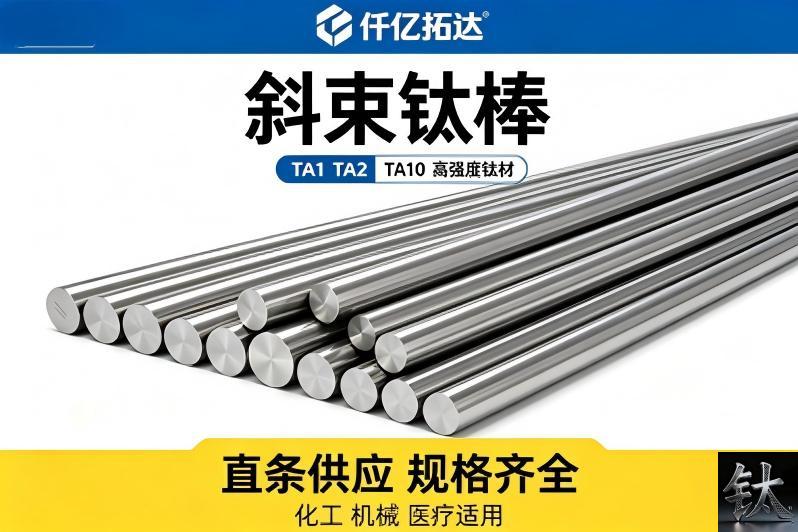
TC4 Titanium Rod for CNC Machining \| Ti-6Al-4V (Gr5) ASTM B348, h7 Ground Blank
| Specification | TC4 titanium rod for CNC machining, Ti-6Al-4V Gr5 rod CNC turning, ASTM B348 TC4 ground bar blank, titanium rod machining parameters 40-80 m/min, h7 TC4 bar CNC lathe, annealed TC4 vs STA machinabilit |
|---|---|
| Reference Price | $30.00 – $35.00 |
Product Description: TC4 titanium rod for CNC machining — Ti-6Al-4V (Gr5) ASTM B348, annealed blank, h7 ground, cut-to-length, heat-traceable EN 10204 3.1. Real machinability notes: 40-80 m/min, sharp carbide, high-pressu
Product Overview
TC4 Titanium Rod for CNC Machining | Ti-6Al-4V (Gr5), Annealed Blank, h7 Ground
Meta Description: TC4 titanium rod for CNC machining — Ti-6Al-4V (Gr5) ASTM B348, annealed blank, h7 ground, cut-to-length, heat-traceable EN 10204 3.1. Real machinability notes: 40-80 m/min, sharp carbide, high-pressure coolant. Quote in 24h.
Overview — A CNC Blank Is Not "a Piece of Rod"
TC4 (Ti-6Al-4V, UNS R56400, 国标 TC4) is the most machined titanium alloy on earth — and one of the easiest to ruin if the blank is wrong. The shop doesn't fail on alloy grade; it fails on:
- Black-bar decarb layer taking the first tool
- Out-of-round dia forcing extra roughing passes
- Saw-cut end not square → first facing pass chatters
- No heat number on the piece → QA kicks the whole lot
Our CNC blank = annealed TC4 + centerless ground OD (h7/h9) + square-faced ends + heat-marked + MTC 3.1. The lathe clamps it; the programmer cuts chips, not scale.
Why Annealed Is the Default CNC Blank
| Condition | UTS | CNC behavior | When to use |
|---|---|---|---|
| Annealed (M) | ≥895 MPa | Best ductility, predictable chip, lower built-up edge | Default for turning/milling/drilling blanks |
| STA (AMS 4965) | ~1170 MPa class | Higher strength, more tool pressure, finer window | Aero forgings, high-load parts — PO-stated heat treat |
| Duplex annealed | Annealed-range | Better fracture toughness | Fatigue-critical structures |
Rule: if the PO doesn't name STA, ship annealed. STA isn't "better for machining" — it's stronger and less forgiving.
Blank Spec We Actually Supply
| Item | Supply |
|---|---|
| Grade | TC4 / Gr5 (Ti-6Al-4V), R56400 |
| Standard | ASTM B348 (industrial); AMS 4928 on request |
| Diameter | Φ3–200mm rotating class; common CNC sizes Φ6/8/10/12/16/20/25/30/40 |
| OD tolerance | h9 centerless ground (default) / h7 (0/-0.015 small dia.) / h6 project |
| Length | 50–6000mm; cut-to-length ±0.5–1.5mm saw; facing → ±0.05mm |
| Ends | As-sawn / deburred / chamfer / CNC face both ends |
| Straightness | ~1mm/m standard; tighter on request |
| Surface | Peeled / centerless ground / Ra≤0.8μm ground / mirror on project |
| Marking | Grade + heat No. + PO ref (laser/etch on request) |
Chemistry (ASTM B348 Gr5, wt%)
| Element | Min | Max |
|---|---|---|
| Ti | Balance | — |
| Al | 5.50 | 6.75 |
| V | 3.50 | 4.50 |
| Fe | — | 0.40 (bar >76mm; smaller sections per edition) |
| O | — | 0.20 |
| C | — | 0.08 |
| N | — | 0.05 |
| H | — | 0.015 (confirm B348 edition) |
Mechanicals (Annealed, Room Temp)
| Property | Value |
|---|---|
| UTS | ≥895 MPa |
| 0.2% YS | ≥828 MPa |
| Elongation | ≥10% |
| Reduction of area | ≥25% |
| Density | 4.43 g/cm³ |
| Modulus | ~114 GPa |
| Thermal conductivity | ~6.7 W/(m·K) — low, hence heat management first |
CNC Machining Notes (Shop-Floor Real, Not Brochure)
TC4 machines fine if you respect three things: sharp tool, low speed, aggressive cooling.
| Operation | Starting window | Note |
|---|---|---|
| Rough turning | 40–60 m/min, f=0.1–0.3 mm/r, ap=1–3mm | YG/ultra-fine carbide; avoid dwell |
| Finish turning | 60–80 m/min, small ap | Ra 0.8–1.6 achievable |
| Milling | Trochoidal / adaptive, low radial engagement | Climb milling; constant chip load |
| Drilling | Short carbide drill, peck cycle | Through-tool coolant strongly preferred |
| Coolant | Semi-synthetic 5–8%; high-pressure 7–12MPa ideal | Flood to chip-tool interface, not just splash |
- Tool: micro-grain carbide, AlTiN/TiAlN PVD; avoid thick Ti-containing coatings that bond with the chip
- No chlorine/sulfur extreme-pressure additives that leave corrosive residue on medical parts
- Rigidity beats RPM: hydraulic/shrink-fit holder, short overhang, soft jaws for thin sections
- Chatter = heat = built-up edge = dimension drift. Stiff fixture first, faster feed second
Blank Prep Options (Pick Before PO)
| Need | Blank config |
|---|---|
| General CNC lathe | h9 peeled + sawn + deburr |
| Precision shaft / pin | h7 ground + face both ends + chamfer |
| Weld-root or seal seat | Saw + CNC facing (perpendicularity reported) |
| 5-axis mill blank | Ground OD + square end + pre-center-drill optional |
| Aerospace | AMS 4928 + UT per spec + dimensional report |
| Medical instrument (non-implant) | ELI route on request; implant = F136/F1472 separate chain |
Traceability for the QA Desk
- One parent heat → all cut blanks carry the same heat No.
- EN 10204 3.1, mill-authorized inspection rep, heat-matched chemistry + tensile
- UT per PO (AMS 4928 level on request, ~Φ0.8mm FBH typical)
- OES spectrum report + tensile on file
- 3.2 (SGS/BV/TÜV) witness at buyer cost, PO-fronted — not retro-signed
- Tag = MTC = crate label
Common CNC Parts From TC4 Blanks
- Aerospace: fasteners, spacers, landing-gear pins, bracket bushings
- Robotics: joint shafts, servo housings, lightweight arms
- Medical (non-implant): instrument handles, surgical tool shafts
- Marine: valve stems, seawater pump shafts
- Racing: bottom brackets, suspension links, fixture blocks
- Industrial: hydraulic pistons, sensor housings, fixture locators
Enquiry Template (Copy-Paste for CNC Buyers)
Grade: TC4 / Gr5 (Ti-6Al-4V) ___
Standard: ASTM B348 / AMS 4928 ___
Diameter: Φ___ mm (h9 / h7 / h6 / per drawing)
Blank length: ___ mm × ___ pcs
Ends: sawn / deburr / chamfer / CNC face both ends
Straightness: ___ mm/m
Surface: peeled / ground Ra≤0.8 / mirror
Pre-op: center-drill? yes/no   chamfer? ___°
Marking: heat No. + PO ref on each piece? Y/N
Cert: 3.1 / 3.2 (TPI: ___)
Machine type: lathe / mill / 5-axis / Swiss
Port: ___ (FOB Shanghai default)
FAQ — TC4 Rod for CNC Machining
Q1: Annealed or STA for my CNC shop?
A: Default annealed — predictable chip, less BUE. STA only if the final part drawing demands ~1170MPa; it costs more tool life.
Q2: Can I machine black bar directly?
A: You can, but you'll burn one roughing tool on scale/decarb. Ground blank pays back in 2–3 parts on repeat runs.
Q3: h7 from stock?
A: Common diameters rotate ground+h7; odd sizes cut+grind to order, lead stated honest.
Q4: Best starting speed?
A: 40–60 m/min rough, 60–80 finish with sharp carbide + high-pressure coolant. Above ~90 m/min tool life drops fast — verify against your insert maker's data.
Q5: Coolant warning?
A: Semi-synthetic, no chlorine/sulfur EP that stains medical parts. High-pressure through-tool > flood > mist.
Q6: Face both ends or just saw?
A: Saw is sizing. If the end seats a bearing or takes a root weld, add CNC facing — perpendicularity becomes a measured value, not a hope.
Q7: Medical implant blank?
A: Industrial TC4 ≠ implant cert. Implant path = Gr23 ELI + F136/F1472 + ISO 13485 traceability, separate PO chain.
Q8: MTC after cutting still valid?
A: Yes — 3.1 ties cut pieces to parent heat; marking locks traceability before the blade drops.
Q9: Dispatch?
A: In-stock ground dia + PO before 3 PM China time → same-week cut/dispatch. Sea FOB Shanghai; air for line-down at buyer cost.
Q10: Trial blank?
A: 1 short cutoff from same heat at courier cost, deductible from bulk PO.
Request a Quote
Email: sales@[yourdomain].com
Send diameter × blank length × qty + end condition. Reply within 24h: live heat, EXW/FOB quote, grind/face scope, MTC type, dispatch date.
About: Baoji Titanium Valley inventory holder. TC4 (Ti-6Al-4V / Gr5) rod for CNC machining — ASTM B348 annealed blank, h7 ground, faced ends on request, heat-number traceable, EN 10204 3.1. We sell the blank your lathe clamps without re-facing — not a 6m guess with scale on it.
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China