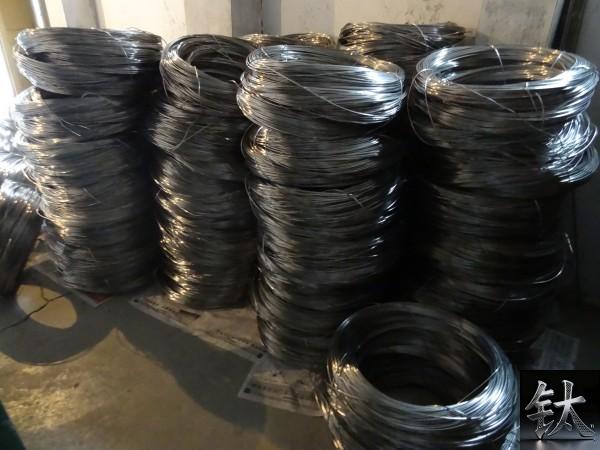
Pure Titanium Wire Gr2 for Chemical Repair \| ERTi-2 AWS A5.16, TIG/MIG, Argon-Clean, MTC 3.1, Baoji Stock
| Спецификация | pure titanium wire Gr2 chemical repair, ERTi-2 AWS A5.16 repair wire, Gr2 titanium vessel weld repair, chloride service titanium filler wire, heat exchanger titanium welding wire, ERTi-2 TIG rod MIG s |
|---|
Описание продукции: Pure Gr2 titanium welding wire for chemical equipment repair — ERTi-2 per AWS A5.16, TIG rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 with measured O/H/N/C. For chloride/brine/heat-excha
Обзор продукции
Pure Titanium Wire Gr2 for Chemical Repair | ERTi-2 AWS A5.16, TIG/MIG, Argon-Clean, MTC 3.1
Meta Description: Pure Gr2 titanium welding wire for chemical equipment repair — ERTi-2 per AWS A5.16, TIG rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 with measured O/H/N/C. For chloride/brine/heat-exchanger/vessel re-welds. Lot confirmed before PI; no ghost shelf, no minima-only cert.
Overview — Repair Welds Fail on Two Things: Wire Identity + Shielding
Chemical plant re-welds on Gr2 shells, tube sheets, and piping are not a "buy any titanium wire" job. The failure modes are predictable:
- Wrong filler class → undermatching/overmatching vs WPS, requalification
- Interstitial pickup (O/N/H) → blue bead, alpha-case, brittle HAZ, delayed crack
- No back purge → root side oxidises, chloride attacks start at the root
- "Minima-only" cert → QA cannot correlate deposit chemistry to WPS
Our Gr2 repair wire is supplied as ERTi-2 per AWS A5.16 — commercially pure, not alloyed, matched to Gr2 base metal for corrosion-service re-welds. Measured interstitials on every MTC 3.1. Lot locked before PI.
Why ERTi-2 for Gr2 Chemical Repair
| Point | Reality |
|---|---|
| Match to base | Gr2 shell/tube/tubesheet → ERTi-2 is the standard filler per WPS; ERTi-1 acceptable where higher ductility is specified |
| Corrosion service | Chlorides, brine, wet Cl₂, seawater, organic acids — CP Ti passive film restored only if weld is clean |
| Strength | UTS ≥345 MPa, YS ≥275 MPa (annealed deposit min) — enough for chemical static equipment |
| Cost | Lower than Gr5, correct choice when strength is not the limiting factor |
| Weldability | GTAW/TIG standard; GMAW/MIG for thicker sections; plasma for long seams |
Note: if the original WPS names ERTi-1, follow the WPS — we supply both, but the WPS decides, not the warehouse.
Chemistry Band (ERTi-2 / AWS A5.16)
| Element | Max / Range |
|---|---|
| Ti | Balance |
| O | ≤0.16% (class band; MTC reports measured value) |
| Fe | ≤0.20–0.30% (per revision) |
| C | ≤0.05% |
| N | ≤0.015% |
| H | ≤0.008% |
MTC 3.1 lists measured O/H/N/C + Fe + tensile — not "complies with max". Repair QA needs numbers, not adjectives.
Repair Scene Stock Menu
| Form | Ø | Use on site |
|---|---|---|
| TIG straight rod | 1.6 / 2.0 / 2.4 / 3.2 mm | Shell patch, tube sheet, root pass, field GTAW |
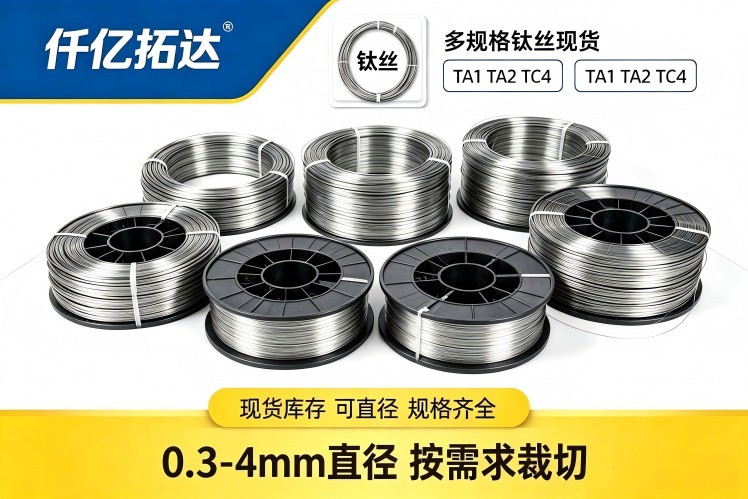
| MIG spool D200 | 0.8 / 1.0 / 1.2 / 1.6 mm | Thick-wall vessel, long seam, automatic carriage |
| Coil (feeder) | 1.0–1.6 mm | Orbital/automatic repair on piping |
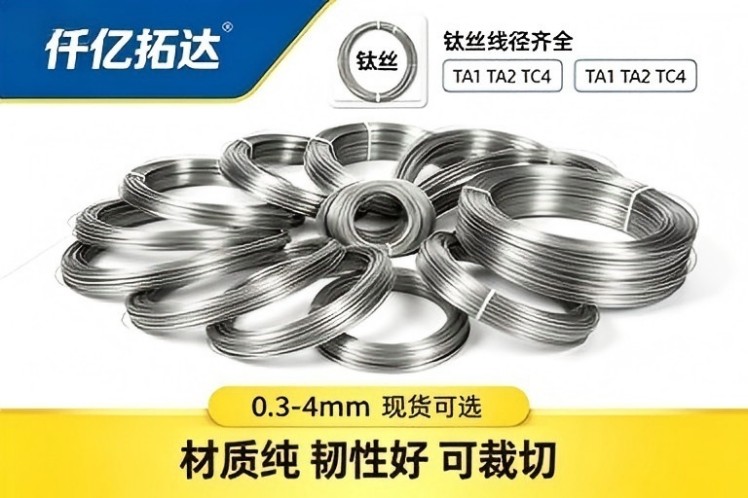
Core Ø 1.6/2.0/2.4mm TIG + 1.2mm MIG on qualified heats — lot confirmed before PI.
Field Repair Discipline (Wire Side + Process Side)
Wire we control; process we align to, we don't pretend to weld for you:
- Argon purity: ≥99.99% (99.995%+ for critical service), dew point ≤-40°C
- Front shield: gas lens / large cup + trailing shield on long seams
- Back purge: root dam / inflatable bladder; keep purging until HAZ <315°C
- Cleaning: acetone/alcohol degrease, dedicated Ti brush only — no steel wool, no carbon-steel tool crossover
- Colour check: silver / light straw = OK; blue/purple = re-clean and redo; alpha-case must be removed
- Wire handling: keep sealed until feed; cut rod ends capped; never lay wire on shop floor
A clean ERTi-2 spool cannot save a leaky purge. We say it upfront so the re-repair ticket doesn't come back to us.
Where It Repairs Well
- Chlor-alkali cells, anode hangers, cathode structures
- Ti tube bundles / shell-and-tube heat exchangers
- Reaction vessels, towers, brine tanks
- Seawater RO / desalination piping
- Paper bleach washers, wet chlorine ducts
- Patch welds on Gr2 shells where WPS permits ERTi-2
Traceability for Repair Records
- Every spool/rod: AWS class + Ø + lot/heat + manufacturer ID flag-tagged
- EN 10204 3.1: measured chemistry + tensile + lot-to-ingot
- Sealed cert pouch with spool; 3.2 (SGS/BV/TÜV) PO-fronted
- ERTi-2 (filler) cert line never merged with B863 base-wire cert
- Pre-ship photo: spool face + seal + lot tag for your shutdown file
Packaging for Site Dispatch
- Vacuum foil + desiccant + aluminium barrier
- TIG rod: PE/kraft tube, ends capped, flag per rod
- MIG: D200 plastic spool, precision layer-wind, no cross-lap
- Outer: plywood case / antistatic carton, "DRY / NO OIL / ARGON-CLEAN"
- Express or air-cargo friendly for shutdown windows
Enquiry Template (Copy-Paste)
Equipment: vessel / heat exchanger / pipe / tubesheet ___
Base metal: Gr2 (confirm WPS) ___
WPS class required: ERTi-2 / ERTi-1 ___
AWS A5.16 rev: ___
Form: TIG rod ___mm / MIG spool ___mm (D200/D300)
Qty: ___ rods / ___ spools
Service fluid: chloride / brine / wet Cl2 / seawater ___
Purge plan: back purge Y/N, argon purity ___
Cert: 3.1 / 3.2 (TPI: ___)
Urgency: shutdown date ___ / sample first ___
Incoterm: EXW Baoji / FOB Shanghai / DAP ___
FAQ — Gr2 Pure Titanium Repair Wire
Q1: ERTi-2 or ERTi-1 for Gr2 repair?
A: Follow the WPS. ERTi-2 is the standard CP filler for Gr2; ERTi-1 where higher ductility is specified. We don't substitute without the WPS line.
Q2: Can it handle chloride service?
A: Yes — CP Gr2/ERTi-2 is chosen for chloride/brine/seawater. But only if the weld stays argon-clean; a contaminated bead loses the passive film locally.
Q3: Blue bead after weld — wire fault?
A: Almost always purge/contamination, not chemistry. Wire ships argon-clean; shielding is site-side. Re-clean HAZ, remove alpha-case, re-weld.
Q4: MTC real numbers?
A: Yes — measured O/H/N/C/Fe + tensile on 3.1. No minima-only stamp for repair orders.
Q5: Fast for shutdown?
A: Core Ø on qualified heats — lot confirmed, same working-week pack after PO. Express/air dispatch supported; tell us the shutdown date in the enquiry.
Q6: STA or annealed?
A: Annealed default. STA is not a repair norm for CP Ti — not pre-shipped, re-heat-treat only on written PO.
Q7: Gr5 equipment — can ERTi-2 repair it?
A: No. Gr5 base → ERTi-5 per WPS. Undermatching needs welding-engineer sign-off. Don't mix.
Q8: Orbital weld wire?
A: 1.0–1.6mm level-wound coil, cast/helix matched to feeder. State push/pull/dual at enquiry.
Q9: Medical/FDA claim?
A: No. This is industrial chemical-repair wire (AWS A5.16), not F136 implant chain.
Q10: Quote time?
A: 24h with WPS class + Ø + form + qty + incoterm. Dispatch date written into quote after lot confirm.
Request a Quote
Email: sales@[yourdomain].com
Send WPS filler class + Ø + form + service fluid + shutdown date. Reply in 24h: live lot No., EXW/FOB price, MTC type, dispatch window.
About: Baoji Titanium Valley repair-wire line for chemical service. Pure Gr2 / ERTi-2 per AWS A5.16 — TIG rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 with measured interstitials. Matched to Gr2 vessels, exchangers, piping in chloride/brine/seawater. Lot locked before PI; shielding discipline is site-side, wire side is ours. No ghost shelf, no "compatible-grade" stamps.
Опишите ваши требования — марка, размер и количество. Ответим в течение 24 часов.
Предпочитаете чат? WhatsApp +86 188 2967 9311 или напишите на sales@sxqytd.com.
- Titanium Price Today (26 октября 2026 г.): отчет о рынке Китая
- Цена на титан сегодня (23 октября 2026 г.): пластина, трубка, стерже
- Читайте титановую проволоку и проволоку из титанового сплава: класси
- Титановая проволока: от выбора марки до производственного процесса (
- Читайте титановую трубку и трубку из титанового сплава: классификаци
Контактное лицо: Wang Xiaoning
Телефон: +86-917-355-7966
Эл. почта: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Компания: Shaanxi Qianyi Tuoda Technology Co., Ltd
Адрес: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China