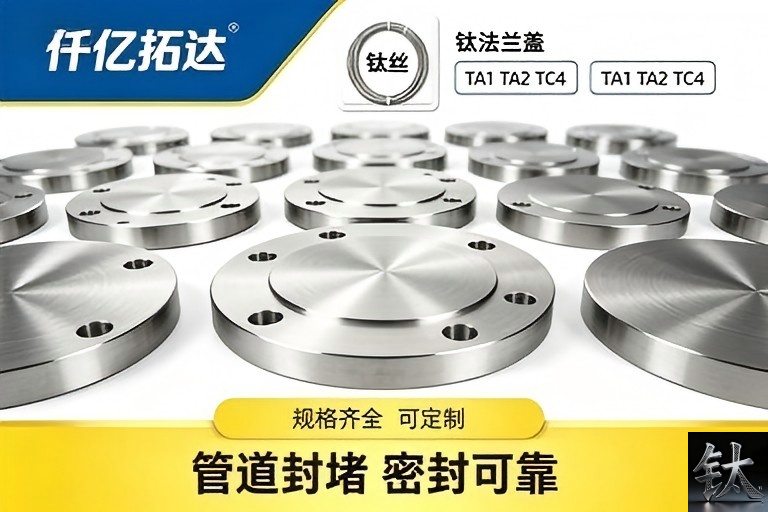
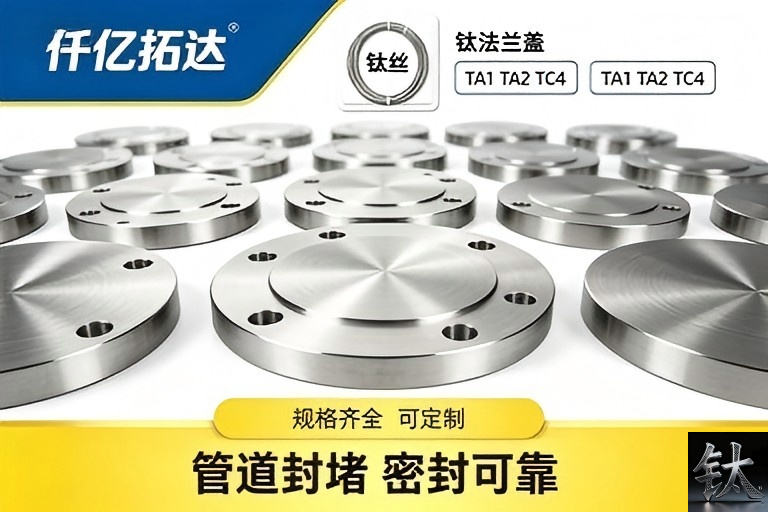
Titanium Flange Cut to Drawing from Inventory \| ASTM B381 F-2/WPT2, Forged Blank + CNC per DWG, B16.5/EN1092/JIS, MTC 3.1, Baoji
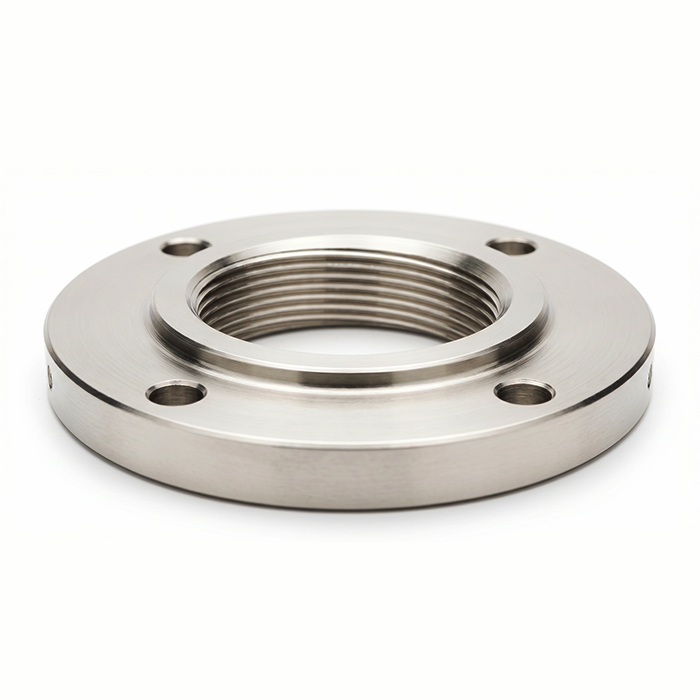
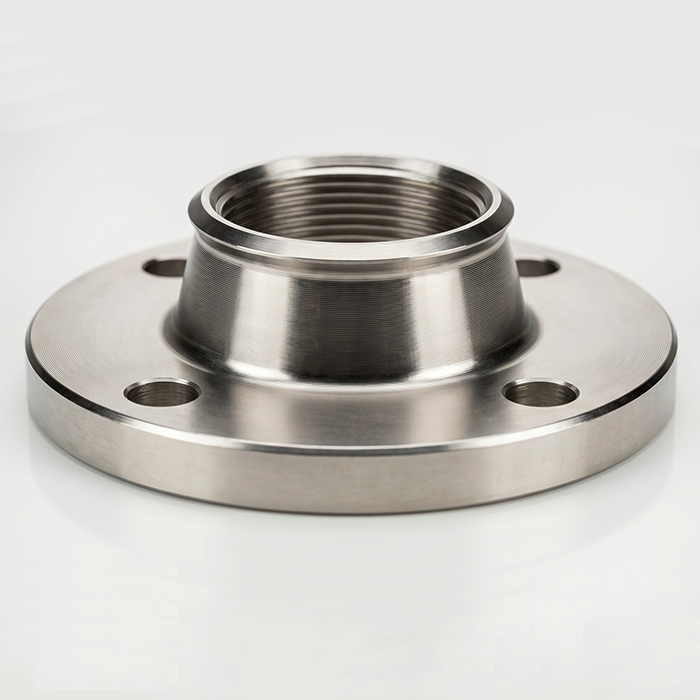
| Specification | We process titanium flanges cut to your technical drawings directly from our in-house titanium stock. Gr1, Gr2, Gr5 and Gr7 blanks are on hand for custom OD, bore and face machining. |
|---|---|
| Applicable Standard | All drawing-machined titanium flanges follow ASME B16.5 and ASTM B381 specifications. We record full inspection data and supply MTC to validate material and dimensional compliance. |
| Material Condition | These custom machined titanium flanges retain outstanding resistance to brine, chloride and acidic media. They fit non-standard piping connections and special equipment flanged joints in corrosive pro |
| Inspection & Packaging | Using existing inventory blanks shortens your lead time greatly. We deliver precision machined flanges with export packing, complete paperwork and technical confirmation before shipment. |
| Reference Price | $20.00 – $60.00 |
Product Description: Titanium flanges cut/machined to drawing from rotating forged inventory — ASTM B381 F-2/WPT2/R50400, Gr5/Gr7/Gr12 on PO, bore/hub/bolt-circle/RTJ groove per your CAD/PDF/isometric. Same heat number ca
Product Overview
Titanium Flange Cut to Drawing from Inventory | ASTM B381 F-2/WPT2, Forged Blank + CNC per DWG
Meta Description: Titanium Flanges machined to drawing from rotating forged inventory — ASTM B381 F-2/WPT2/R50400, Gr5/Gr7/Gr12 on PO, bore/hub/bolt-circle/RTJ groove per CAD/PDF/isometric. Same heat carried billet→finished flange; EN 10204 3.1, PMI, UT/PT.
What "From Inventory" Actually Means Here
Not "we have your exact non-standard flange on a shelf" — that would be dishonest. It means:
- Certified titanium forged blank / rough-turned ring from a confirmed rotating heat (Gr2 default, Gr5/Gr7/Gr12 PO-grade)
- B381 forging route already done: billet → forge → anneal → rough machine
- Your drawing drives the finish CNC stage only: bore, hub taper, facing, bolt-circle, RTJ groove, counterbore, special thickness
- Heat number etched before machining starts — never reassigned
Result: non-standard geometry without re-melting or waiting for a new forge campaign.
What We Machine per Drawing
- Custom bore to pipe SCH (5S/10S/40S/80S/XXS) or full-diameter
- Non-B16.5 bolt circle / PN-DIN drill / JIS B2220 / HG-T pattern
- RTJ groove to spec, tongue-groove, M&F, extended hub, long weld neck
- Eccentric/reducing flange, orifice flange, spectacle blind companion
- Special thickness, facing finish (Ra control), counterbore, seal chamber
- CAD / PDF / STEP / isometric + gasket dwg all accepted
Standards Covered
- Material: ASTM B381 / ASME SB381 (F-2/F-5/F-7/F-12)
- Dim base: ASME B16.5 (NPS 1/2–24), B16.47 Series A/B for large bore
- Alternate: EN 1092-1, DIN 2627–2638, JIS B2220, GB/HG on request
- Class: 150–2500 (class fixes dimensions/bolt pattern; working pressure calculated per grade+T)
Process Chain (traceability intact)
- Confirm rotating heat No. from forged blank stock
- DFM check: drawing vs forge envelope (hub length, min thickness)
- CNC turn/bore/drill/groove per DWG
- Anneal stress-relief if cold-cut depth triggers code review
- Pickle descale, face protect, re-etch heat No.
- MTC 3.1: parent heat chemistry + finish-dim report + NDE
Parent heat = finished-flange heat. Drawing changes geometry, not metallurgy.
Lead-Time Logic (honest)
| Case | Typical window |
|---|---|
| Gr2 WN/Blind, small bore, confirmed blank | CNC slot in working week after lot confirm |
| Custom bore + RTJ + non-B16.5 drill | +CNC queue, quoted per dwg |
| Gr5/Gr7 project heat / large bore | forge slot PO-fronted, schedule quoted |
| Prototype 1pc | handled; no tonnage gate |
We quote the window after seeing the drawing + confirming blank — not before.
Drawing RFQ Checklist
Attached: CAD/PDF/STEP ___
Type: WN / SO / Blind / LJ / Orifice / LWN ___
Grade: Gr2 (F-2/WPT2/R50400) / Gr5 / Gr7 / Gr12 ___
NPS & bore (SCH): ___
Class / standard: B16.5 300# / EN1092 PN16 / JIS 10K ___
Facing: RF / FF / RTJ (groove dwg) / T&G ___
Bolt holes: Qty + PCD + hole Ø + tap? ___
Special: hub length / counterbore / thickness / Ra ___
Qty: ___ pcs
Cert: 3.1 / 3.2 (TPI ___)
Incoterm: EXW Baoji / FOB Shanghai / DAP ___
Inspection & Cert
- PMI/XRF grade verify (Gr7 Pd by chemistry)
- UT on forging, PT on machined face
- CMM/dial dim report vs drawing datums
- EN 10204 3.1: parent-heat chemistry + tensile, QA-signed
- 3.2 (SGS/BV/TÜV/DNV) PO-fronted — not back-built after machining
When This Route Beats Full Standard Stock
- Isometric bore doesn't match SCH 40S default
- Existing equipment drilled to old DIN/PN pattern
- RTJ groove or orifice tap not in catalogue
- Spare flange must match a 10-year-old line exactly
- Prototype before full project award
When It Is NOT the Right Route
- Pure standard B16.5 RF Class300 → use stock page, faster/cheaper
- HF / dry chlorine / red fuming nitric → titanium excluded, stop before quote
- No drawing, "make it fit" → we DFM-review first, never blind-cut
FAQ — Titanium Flange Cut to Drawing from Inventory
Q1: Is it really "from inventory"?
A: Forged blank from a confirmed rotating heat — CNC finish per your dwg. Not a finished standard flange waiting on shelf, but no re-melt either.
Q2: Does heat number stay valid after machining?
A: Yes. Geometry changes; metallurgy doesn't. Parent heat = finished heat, re-etched post-machine.
Q3: Which files do you need?
A: CAD/STEP preferred; clean PDF with dims + tolerance + facing detail works.
Q4: Can you copy an old flange with no drawing?
A: Yes — send the sample or full-dim sketch; we reverse-measure, issue DFM, then machine.
Q5: Gr2 enough?
A: Ambient–moderate seawater/oxide service yes. Hot crevice brine → Gr7/Gr12 review before cut.
Q6: Tolerance?
A: B16.5 datums standard; tighter bore/face Ra by dwg, typical CNC ±0.02–0.1mm by feature.
Q7: RTJ groove ok?
A: Machined to groove dwg / B16.5, not hand-finished.
Q8: 1-piece prototype?
A: Handled. No moq wall for drawing jobs.
Q9: 3.2 possible?
A: TPI at PO stage; witnesses forge+NDE. Cannot be retro from 3.1.
Q10: HS code?
A: WCO 6-digit 8108.90 base; destination sub-heading via broker. Process statement supplied.
Request a Quote
Email: sales@[yourdomain].com
Attach drawing + grade + qty. Reply in 24h: blank heat status, DFM note, EXW/FOB price, machine slot, dispatch window.
About: Baoji Titanium Valley drawing-flange line — ASTM B381 F-2/WPT2 forged blank → CNC per CAD/PDF, ASME B16.5/EN1092/JIS, RF/RTJ/T&G, heat-carried, pickle-finished, EN 10204 3.1. Non-standard bore/hub/drill without re-melting. No heat reassign, no cast substitute, no cert downgrade. Lot confirmed before PI; tag = MTC = PL.
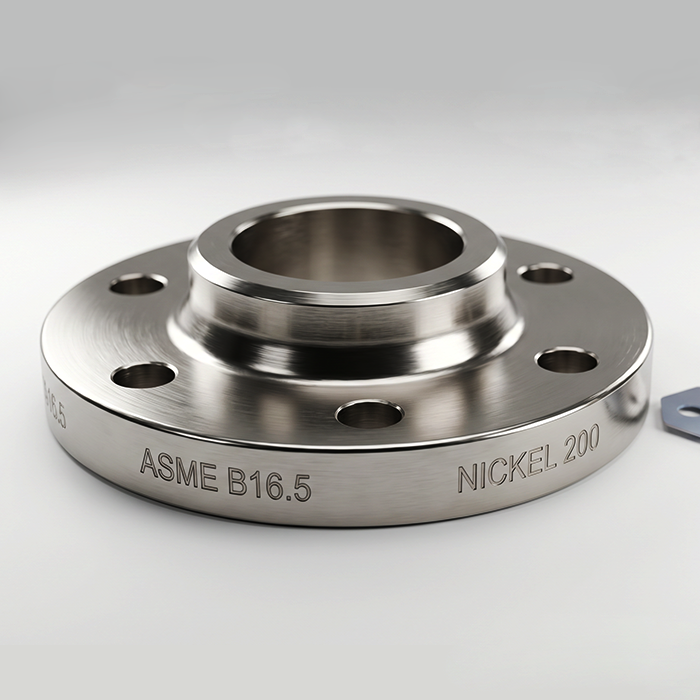
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
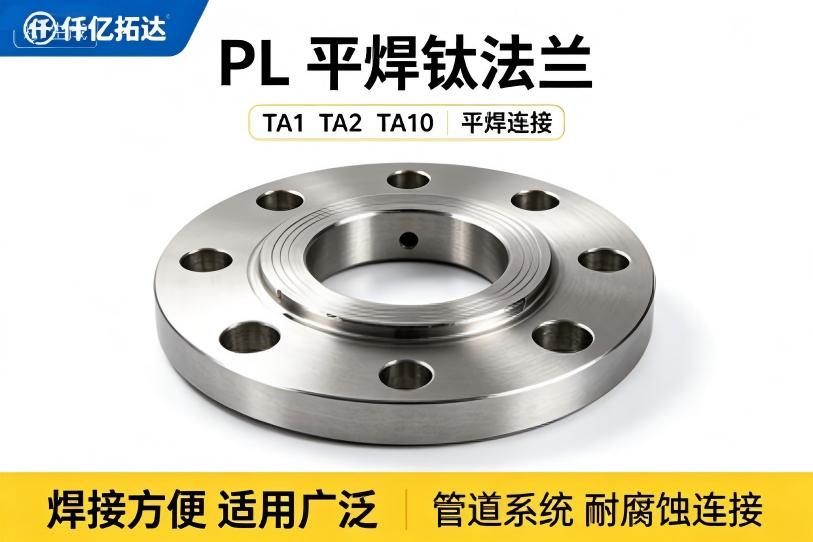
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China