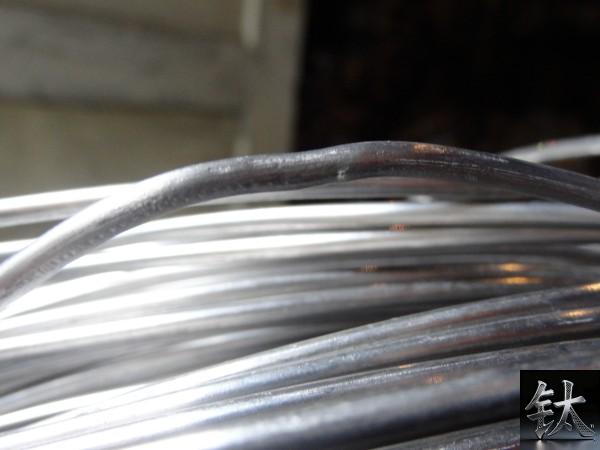
TC4 Titanium Wire for Additive Manufacturing \| Ti-6Al-4V (Gr5) WAAM/LMD/DED Feedstock, VAR, Ø0.8–1.6mm Spool, MTC 3.1
| Specification | TC4 titanium wire additive manufacturing, Ti-6Al-4V WAAM wire, Gr5 DED feedstock spool, LMD titanium wire 1.2mm, EBAM TC4 wire, ASTM B863 F3183 titanium AM wire, VAR Ti-6Al-4V wire Baoji, additive man |
|---|
Product Description: TC4 titanium wire additive manufacturing, Ti-6Al-4V WAAM wire, Gr5 DED feedstock spool, LMD titanium wire 1.2mm, EBAM TC4 wire, ASTM B863 F3183 titanium AM wire, VAR Ti-6Al-4V wire Baoji, additive man
Product Overview
TC4 Titanium Wire for Additive Manufacturing | Ti-6Al-4V (Gr5) WAAM / LMD / DED Feedstock, VAR, MTC 3.1
Meta Description: TC4 (Ti-6Al-4V) wire for additive manufacturing from Baoji — WAAM/LMD/DED/EBAM feedstock, VAR double melt, Ø0.8–1.6mm precision spool, ±0.02–0.03mm, bright-clean, low interstitials, EN 10204 3.1 lot-traceable. Deposited properties quoted per process, not brochure minima.
Overview — AM Wire Is Not Welding Wire
If you quote a TC4 AM project with "ERTi-5 welding wire", QA will kick it back. Wire-fed additive manufacturing consumes metal differently:
- Welding wire = arc stability + clean bead
- AM feedstock wire = uninterrupted feed + zero surface carbon/oil + tight cast/helix + interstitial ceiling + lot-to-deposit traceability
A poriferous print rarely comes from "bad titanium" — it comes from oil residue, hydrogen pickup, diameter drift, or cross-lapped spool tangling the feeder at layer 40. We supply TC4 (Ti-6Al-4V, R56400) as additive feedstock: VAR double melt, bright-annealed, roller-die drawn, precision layer-wound, lot-closed. Annealed condition default; STA/hip-post per build procedure, not pre-shipped as "finished properties".
Why TC4 for Wire AM
- α+β workhorse: strength-to-weight ~2× 304SS at equal mass
- WAAM deposition 1–4 kg/h on meter-scale structures (spar, rib, housing, nozzle preform)
- LMD/DED: localized cladding, repair, hybrid CNC+print
- EBAM: large near-net aerospace forgings without powder handling
- Post-anneal recovers near-wrought ductility; STA available PO-stated
Rule: large, low-volume, high-buy-to-fly-ratio parts → wire AM beats billet CNC on scrap. Micro-resolution medical lattice → powder bed, not wire.
Process × Diameter Map (TC4)
| Process | Common Ø | Note |
|---|---|---|
| WAAM (GTAW/GMAW arc) | 1.2 / 1.6 mm | Mainstream; 1.2mm fine-bead, 1.6mm high deposition |
| LMD (laser wire) | 0.8 / 1.0 / 1.2 mm | Laser spot-matched; 1.2mm most cited in LMD cases |
| DED / cold metal transfer AM | 1.0–1.6 mm | Cast/helix tight = no birdnest |
| EBAM | 1.2–2.0 mm project | Chamber feed; PO-stated spool/core |
Diameter tolerance: ≤1.5mm ±0.02mm typical; 1.6mm ±0.03mm class. Final tolerance written in PO.
Stock Scope (Honest)
| Item | Supply |
|---|---|
| Grade | TC4 / Gr5 (R56400); Gr23 ELI (R56401) on separate PO for fracture-critical |
| Ø | 0.8 / 1.0 / 1.2 / 1.6 mm (2.0mm on project) |
| Spool | D200 (5kg) / D300 (10kg) / custom wind to feeder model |
| Condition | Annealed (M) default; STA/hip per build procedure (PO-fronted) |
| Surface | Bright annealed + pickled + ultrasonic degrease, no graphite lube |
| Standards referenced | ASTM B863 / AWS A5.16 (ERTi-5 class) / AMS 4954; AM-specific clauses (F3183-family / ISO-ASTM 52941 / AMS700x) cited per customer PO |
Honest line: common 1.2/1.6mm D200 rotate on qualified heats. ELI / STA / EBAM core / custom wind → melt schedule quoted before PI. No "any spec same-day".
Interstitial Control — The Real AM Spec
| Element max | TC4 (Gr5) AM target | Why it matters in print |
|---|---|---|
| O | ≤0.20% (AWS A5.16 ERTi-5 filler class); AM lot tightened per PO | Over-O = stronger but brittle; ductility drops |
| H | ≤0.005% (rod class); vacuum anneal to suppress H pickup | Hydrogen embrittlement / cold-crack in deposit |
| N | ≤0.03–0.05% | Nitrided surface = hard, brittle skin |
| C | ≤0.03–0.08% | Carbide stringers hurt fatigue |
| Fe | ≤0.40% | β-stabilizer, controlled |
| Al / V | 5.5–6.75 / 3.5–4.5% | Phase balance = printability |
MTC lists measured O/H/N/C — not "complies". That is what lets you correlate wire lot → deposit CTQ.
Feedstock Physical Spec (What Printers Actually Feel)
- Diameter tol: ±0.02mm (≤1.5mm) / ±0.03mm (1.6mm)
- Cast (coil set): controlled radius, no tight kinks
- Helix: minimal; straightness on straight-feed variant <2mm/m
- Layer wind: precision, edge-controlled, no cross-lap / no overlap
- Surface: Kodak gray ≤Grade 3 class cleanliness; no oxide scale, no drawing lube
- EdDY/UT on PO for >3mm; visual + dia-scan 100% on AM spool lots
Deposited Properties — Quoted Per Process, Not Brochure
| Condition | UTS | YS | Elong |
|---|---|---|---|
| As-built (WAAM, typical) | 900–950 MPa | 850–900 MPa | 8–12% |
| Annealed post-print | 950–1000 MPa | 880–950 MPa | 10–14% |
| Annealed base wire (M) | ≥895 MPa | ≥828 MPa | ≥10% |
Numbers are process-referenced ranges from WAAM/LMD practice, not a guarantee on your machine. Final deposit properties = your parameter window + post-heat + our lot MTC correlated together.
Gas & Process Notes (Printer-side)
- Shielding: Ar ≥99.99% (WAAM/LMD), chamber vacuum for EBAM
- Interpass 150–300°C controls residual stress (WAAM reference)
- No oil, no glove print on wire — open spool at clean feeder only
- Vacuum-foil + desiccant pack; reseal half-used spool
- Density target ≥99.5% with correct purge + power — wire can't fix a leaky chamber
Traceability Chain
- VAR double melt (triple on request) — ingot pedigree on MTC
- Lot-to-ingot heat No. across spool → deposit coupon
- EN 10204 3.1, mill-authorized IR: chemistry (interstitials called out) + tensile + cast/helix report
- 3.2 (SGS/BV/TÜV) witness PO-fronted, not back-signed
- Gr23 ELI AM = separate PO, F136/ISO 5832-3 chain, never mixed with industrial TC4
Packaging
- D200/D300 plastic spool, vacuum foil + desiccant + aluminium barrier
- "ARGON-CLEAN / NO OIL / DRY" outer label
- Plywood case / antistatic carton, spool face protected
- Pre-ship photo: spool face + lot tag + seal
Enquiry Template (Copy-Paste for AM Engineers)
Grade: TC4(Gr5) / Gr23 ELI ___
Process: WAAM / LMD / DED / EBAM ___
Diameter: 0.8 / 1.0 / 1.2 / 1.6 mm ___
Tolerance: ±0.02 / ±0.03 / per drawing
Spool: D200 / D300 / custom wind (feeder model: ___)
Weight: 5kg / 10kg / ___ kg
Condition: annealed / STA-PO / hip-PO
Surface: bright annealed / pickled
Interstitial cap: O___% H___ppm N___%
Standard cited: ASTM B863 / AWS A5.16 ERTi-5 / AMS4954 / F3183-family / ISO-ASTM 52941 ___
Cast/helix: stated ___ / "AM-grade controlled"
Cert: 3.1 / 3.2 (TPI: ___)
Qty: ___ spools
Incoterm: EXW Baoji / FOB Shanghai / DAP ___
FAQ — TC4 Wire for Additive Manufacturing
Q1: Can I use ERTi-5 welding wire for WAAM?
A: Technically feedable, but AM feedstock needs tighter cast/helix, lower surface carbon, and lot-to-deposit traceability. We supply TC4 as AM-grade, not relabeled MIG wire.
Q2: Best diameter for LMD?
A: 1.2mm is the mainstream laser-wire size; 0.8–1.0mm for fine-bead. Match to laser spot + powder-free nozzle, not "thinner = better".
Q3: Does annealed wire print at 895 MPa?
A: No. Base-wire UTS is annealed-minimum. As-built deposit runs ~900–950 MPa, rises to ~950–1000 MPa after anneal, depending on your heat input. We correlate lot MTC + your WPQ.
Q4: STA from stock?
A: No. Annealed default. STA/hip done per build procedure + PO, with re-MTC. Never pre-ship "print-ready STA properties".
Q5: Porosity in print — wire fault?
A: Often not. Leaky chamber, bad argon dewpoint, oil on guide tube cause it. Wire must be clean; process must be clean. We ship argon-sealed, you keep it sealed.
Q6: Gr23 ELI for AM?
A: Yes for fracture-critical / medical-adjacent. Lower O (≤0.13%), better fatigue, separate PO + F136 chain.
Q7: Spool tangling?
A: Precision layer-wind to feeder type (push/pull/dual). State feeder model — we wind, not just load.
Q8: UT on wire?
A: Eddy + dia-scan 100% on AM lots; volumetric UT on >3mm per PO. Acceptance threshold in contract, not "zero defect".
Q9: EBAM supply?
A: 1.2–2.0mm core/spool PO-fronted; chamber-feed pack agreed before dispatch.
Q10: Lead time?
A: 1.2/1.6mm D200 on qualified heats → same-week after PO+lots confirmed. ELI/STA/custom wind → melt schedule quoted before PI.
Request a Quote
Email: sales@[yourdomain].com
Send process + Ø + spool + condition + cited standard. Reply in 24h: lot No., EXW/FOB price, MTC type, dispatch date.
About: Baoji Titanium Valley AM-feedstock supplier. TC4 (Ti-6Al-4V) wire for WAAM / LMD / DED / EBAM — VAR double melt, bright-annealed, ±0.02–0.03mm, low interstitials, EN 10204 3.1 lot-traceable ingot-to-deposit. Not relabeled welding wire. Annealed default; print properties quoted with your process, not claimed from a brochure.
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China