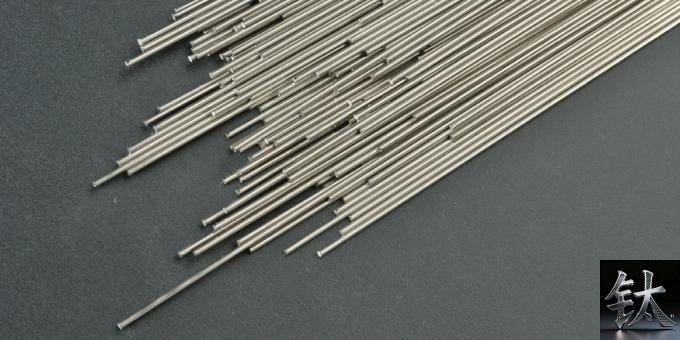
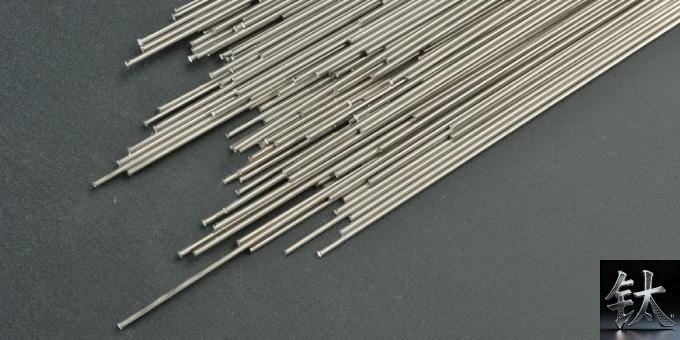
Nickel Welding Rod Ready Stock Baoji
| Specification | ERNi-1 nickel TIG rod AWS A5.14 N02061 ready stock caustic Baoji MTC 3.1 / pure nickel welding wire spool ENi-1 electrode for N02200 N02201 |
|---|---|
| Applicable Standard | ERNi-1 nickel TIG rod AWS A5.14 N02061 ready stock caustic Baoji MTC 3.1 / pure nickel welding wire spool ENi-1 electrode for N02200 N02201 |
| Material Condition | ERNi-1 nickel TIG rod AWS A5.14 N02061 ready stock caustic Baoji MTC 3.1 / pure nickel welding wire spool ENi-1 electrode for N02200 N02201 |
| Inspection & Packaging | We provide clean, oil-free packaging to protect rod surfaces from contamination, support combined shipment with nickel plates, pipes and fittings, and deliver full export documents for industrial weld |
| Reference Price | $40.00 – $60.00 |
Product Description: Ready-stock nickel welding consumables from Baoji — ERNi-1 bare rod/wire (AWS A5.14, UNS N02061) for GTAW/GMAW/SAW, plus ENi-1 (AWS A5.11) coated electrodes for SMAW, matched to Nickel 200 (N02200) /
Product Overview
nickel rod for Welding, Ready Stock Baoji | ERNi-1 TIG/MIG + ENi-1 Electrode for Nickel 200/201
Meta Description: Ready-stock nickel welding consumables from Baoji — ERNi-1 bare rod/wire (AWS A5.14, UNS N02061) for GTAW/GMAW/SAW, ENi-1 (AWS A5.11) coated electrodes for SMAW, matched to Nickel 200 (N02200) / 201 (N02201). Caustic duty, heat-number traceability, EN 10204 3.1.
Rod vs Filler — Say It Once, Correctly
- Base metal rod/bar: Nickel 200 = UNS N02200, Nickel 201 = UNS N02201 (ASTM B160 / SB-160)
- Matching bare filler (TIG/MIG): ERNi-1, AWS A5.14 / ASME SFA-5.14, UNS N02061
- Matching coated electrode (SMAW): ENi-1, AWS A5.11
- ERNi-1 is NOT N02200 — it carries 2-3.5% Ti to tie up free carbon and control porosity; deposit Ni ≥93%
- Do not substitute 308L/316L stainless filler on pure nickel — wrong system, hot-crack risk
Ready-Stock Window (typical)
| Form | Diameter | Pack | Process |
|---|---|---|---|
| TIG straight rod | 1.6 / 2.0 / 2.4 / 3.2 / 4.0 mm | 5 kg tube, 1000 mm length | GTAW (DCEN, 100% Ar) |
| MIG wire | 0.8 / 1.0 / 1.2 / 1.6 mm | 15 kg spool | GMAW (Ar or Ar+25%He) |
| Coated electrode | 2.5 / 3.2 / 4.0 mm | sealed pack | SMAW (ENi-1) |
| SAW coil | 1.6 / 2.4 mm | 25 kg coil + matched flux | Submerged arc |
Live stock confirmed by heat lot — send diameter + process + qty, reply within 4 business hours.
Why ERNi-1 for Caustic Plants
- Matches corrosion behavior of N02200/N02201 in NaOH/KOH
- Ti deoxidizes weld pool → low porosity, sound root pass
- Low free-carbon deposit → compatible with low-carbon 201 base (no graphite embrittlement path)
- Joins nickel-to-nickel, nickel-to-carbon steel, stainless, Monel, Cu-Ni (transition/buffer layer)
- No preheat needed; PWHT usually not mandatory unless WPS calls for stress relief
The 315°C Rule (written on every quote)
- Base metal ≤315°C → Nickel 200 (N02200) + ERNi-1
- Base metal >315°C (hot caustic evaporator) → Nickel 201 (N02201) + ERNi-1, low-carbon route
- Welding heat cycle can push 200 into graphitization risk — high-temp service defaults to 201 base + ERNi-1
Welding Discipline (shop floor reality)
- Mechanically clean + acetone/degrease; no sulfur, lead, oil, copper residue
- 100% argon backing on root pass (GTAW)
- Interpass ≤150°C (complex parts ≤100°C)
- No oxy-acetylene welding (carburization)
- No stainless brush — nickel-dedicated tools only, prevent iron contamination
- Post-weld: pickle if heat tint present; light stress relief 550-650°C on high-restraint joints per WPS
QC / Docs With Every Lot
- EN 10204 3.1 MTC — heat number, chemistry, all-weld-metal tensile
- Lot ID per AWS A5.02 / SFA-5.02 (spool-to-heat traceability)
- PMI spot on bare rod; diameter laser gauge 100%
- Sealed anti-moisture pack (electrodes baked/conditioned per class)
- 3.2 (SGS/BV/TÜV) TPI PO-fronted, not back-built
- Dual cert AWS A5.14 + ISO 18274 available
RFQ Template (copy-paste)
Filler type: ERNi-1 TIG rod / MIG wire / ENi-1 electrode / SAW coil ___
Diameter: ___mm
Process: GTAW / GMAW / SMAW / SAW ___
Base metal: N02200 (≤315°C) / N02201 (>315°C) / dissimilar(__) ___
Service: NaOH ___% + temp ___°C
Qty: ___ kg / ___ spools
Pack: 5kg tube / 15kg spool / sealed electrode box ___
Cert: 3.1 / 3.2 (TPI ___) / dual AWS+ISO ___
WPS attached: Y/N
Incoterm: EXW Baoji / FOB Shanghai / DAP / DDP ___
FAQ — Nickel Welding Rod, Ready Stock
Q1: Is ERNi-1 the same as Nickel 200?
A: No. N02200 is base metal; ERNi-1 (N02061) is the filler, with Ti added. Same corrosion family, different UNS — MTC states both clearly.
Q2: Can I use 316L wire on nickel?
A: No. Wrong alloy system — hot cracking, loss of caustic resistance. Pure nickel needs pure-nickel filler (ERNi-1 / ENi-1).
Q3: TIG or MIG for field repair?
A: TIG (ERNi-1 straight rod) for root + precision; MIG for production runs. Both 100% argon shield.
Q4: 200 base or 201 base for my evaporator?
A: ≤315°C → 200; >315°C → 201 base + ERNi-1. We flag grade before pricing.
Q5: Electrode storage?
A: ENi-1 packs sealed; re-condition per AWS class if moisture-exposed — never weld from a damp pack.
Q6: Small maintenance qty OK?
A: Yes — 5 kg TIG tube or single spool handled, not ton-only.
Q7: MTC with consumable?
A: EN 10204 3.1 every lot; heat-to-spool traceable. 3.2 TPI PO-fronted.
Q8: Dissimilar joint (Ni to CS)?
A: ERNi-1 buffer layer is the standard route; WPS/PQR must qualify F-No.41 filler per ASME IX.
Q9: HS code?
A: Nickel welding consumable base 7505.22 / 7505.11 band — Broker confirms by destination.
Q10: Biggest mistake buyers make?
A: Buying "pure nickel rod" without UNS on the cert — if the MTC doesn't show N02061 (filler) or N02200/201 (base), reject it.
Request a Quote
Email: sales@[yourdomain].com
Send diameter + process (TIG/MIG/SMAW) + base grade + service temp + qty. Stock confirm in 4h; dispatch window after heat lock.
About: Baoji nickel-welding consumable desk — ERNi-1 (AWS A5.14, UNS N02061) TIG rod / MIG wire / SAW coil + ENi-1 (AWS A5.11) electrodes, matched to Nickel 200 (N02200) / 201 (N02201) base metal. Caustic/NaOH duty, 315°C grade rule applied, heat-number traceability, EN 10204 3.1, dual AWS+ISO cert on request. No stainless filler substitution, no "mystery pure nickel", no moist-pack dispatch. Lot = heat = MTC.
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China