ASTM B863 Titanium Wire & Welding Wire: ERTi Grades, Forms & RFQ Guide
ASTM B863 Titanium Wire & Welding Wire: ERTi Grades, Supply Forms & Procurement Guide

Table of Contents
- 1. What Is ASTM B863?
- 2. ASTM B863 vs. AWS A5.16: Mill Product vs. Welding Filler
- 3. B863 Grades vs. ERTi Classifications
- 4. Spool, Coil, Straight Length, Bright Annealed
- 5. Diameter Range, Tolerances & Cast/Helix
- 6. Surface Finish: Pickled, Bright, Polished
- 7. ET, UT, Chemistry, Hydrogen Control & MTR
- 8. How to Write an ASTM B863 / ERTi RFQ
- 9. Wire Procurement Mistakes That Ruin Welds
- 10. Our Wire, Filler & Welding Support
- 11. FAQs
- 12. Related Standards
1. What Is ASTM B863?
ASTM B863 is the standard specification for titanium and titanium alloy wire. It covers wire supplied as coil, spool, or straight length for welding filler metal, springs, fasteners, mesh, medical components, and additive-manufacturing feedstock.
The ASME version is SB-863. But here is the trap buyers fall into:
ASTM B863 = the wire product.
AWS A5.16 / ASME SFA-5.16 = the welding-filler classification.
A wire can be made to B863 and still need an ERTi classification before you put it in a TIG torch.
2. ASTM B863 vs. AWS A5.16: Mill Product vs. Welding Filler
| Item | ASTM B863 | AWS A5.16 / SFA-5.16 |
|---|---|---|
| Type | Mill product standard | Welding consumable standard |
| Names | Gr.1, Gr.2, Gr.5, Gr.23… | ERTi-1, ERTi-2, ERTi-5, ERTi-23… |
| Used for | Wire, rod, spring, fastener, AM feedstock | TIG / MIG / GTAW / GMAW filler metal |
| Focus | Diameter, condition, chemistry, mechanicals | All-weld-metal chemistry, weldability, purity |
| Procurement rule | “B863 Gr.2 wire” is OK for industrial wire | Welding PO should say “ERTi-2 per AWS A5.16” |
If the wire goes into a weld pool, write both:ASTM B863 Gr.2, ERTi-2 per AWS A5.16. That removes ambiguity at incoming inspection. [1,7](@ref)
3. B863 Grades vs. ERTi Classifications
| B863 Grade | ERTi Class | Why use it | Typical use |
|---|---|---|---|
| Gr.1 | ERTi-1 | Lowest interstitials, best ductility | CP Ti cladding, chemical weld root pass |
| Gr.2 | ERTi-2 | Most common industrial filler | Gr.2 pipe, vessel, exchanger welding |
| Gr.5 | ERTi-5 | Ti-6Al-4V, high strength | Aerospace brackets, Ti-6Al-4V structures |
| Gr.7 | ERTi-7 | Pd-added corrosion resistance | Reducing-acid process equipment |
| Gr.9 | ERTi-9 | Ti-3Al-2.5V, strength + formability | Aerospace hydraulic tubing welds |
| Gr.12 | ERTi-12 | 0.3Mo-0.8Ni, hot chloride resistance | FGD, geothermal, chemical piping |
| Gr.23 | ERTi-23 / ERTi-5ELI | ELI, medical implant grade | Implants, orthodontics, surgical wire |
Rule of thumb: match filler to base metal family. ERTi-2 welds Gr.1/Gr.2; ERTi-5 welds Gr.5; ERTi-23 welds Gr.23. Don’t weld Gr.5 structure with ERTi-2 — you lose strength in the weld metal. [2,4](@ref)
4. Spool, Coil, Straight Length, Bright Annealed
- Spool wire: 0.8–2.4 mm common for TIG/MIG/WAAM; 5–15 kg spools
- Coil wire: cost-effective for drawn wire and industrial forming
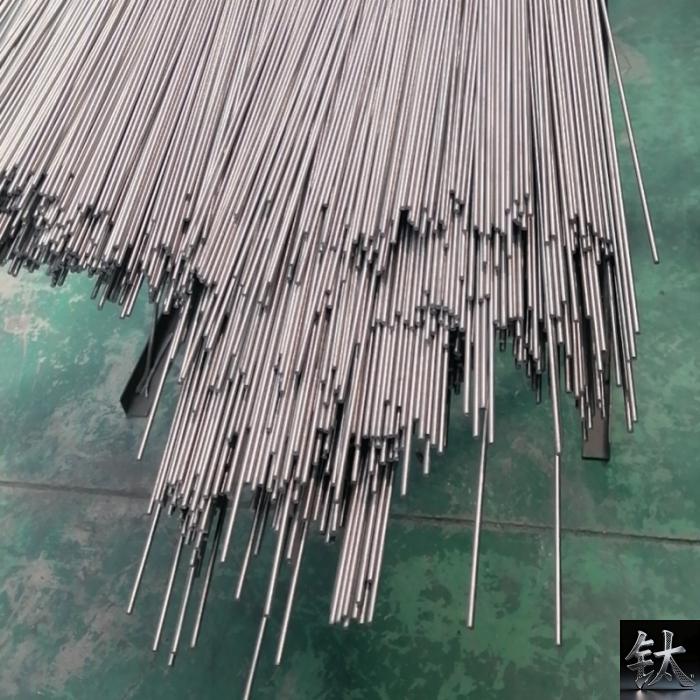
- Straight length / welding rod: 500 mm, 914 mm, 1000 mm cut rods for GTAW
- Bright annealed: vacuum/inert annealed, low oxide, critical welding
- Annealed soft: springs, forming, medical bending
- Cold-worked hard: fasteners, high-tensile small parts
For automatic TIG/MIG, specify cast and helix — bad cast causes bird-nesting in the torch.
5. Diameter Range, Tolerances & Cast/Helix
- Diameter range: 0.1 mm to 8.0 mm typical; heavier rod/straight stock wider
- Fine wire: ±0.013 mm class tolerance for small diameters
- Larger wire: ±0.05 mm class tolerance common
- Ovality: ≤ 50% of total diameter tolerance
- Straight lengths: straightness and cut-square ends matter
- Spool wire: package weight, winding tension, cast/helix agreed upfront
| Diameter | Common tolerance | Form |
|---|---|---|
| 0.1–0.5 mm | ±0.013 mm class | Spool / AM feedstock |
| 0.8–2.4 mm | tight spool tolerance | TIG / MIG filler |
| 2.4–4.0 mm | straight-rod tolerance | GTAW rods |
| 4.0–8.0 mm | ±0.05 mm class | Spring / fastener / straight wire |
6. Surface Finish: Pickled, Bright, Polished
| Finish | Ra / look | Use |
|---|---|---|
| Pickled / chemically cleaned | Matte, oxide-free | Standard welding wire, chemical service |
| Bright annealed | 0.2–0.4 µm, metallic bright | Critical TIG, aerospace, medical |
| Polished | 0.1–0.3 µm | Medical archwire, jewelry, eyewear |
| As-drawn / black | Drawing oxide present | Non-critical forming, later cleaned |
For titanium welding, “clean” beats “shiny”. Any embedded iron, oxide, or oil causes porosity, hardening of the weld, or contamination. [2,3](@ref)
7. ET, UT, Chemistry, Hydrogen Control & MTR
- Chemical analysis: Ti balance; Fe/O/N/C/H + alloying elements per grade
- Hydrogen control: often held very low for weld-integrity grades
- Tensile: UTS, YS, elongation in supplied condition
- ET: surface crack / seam detection for fine and spool wire
- UT: used for larger wire/rod where agreed
- Bend test: optional, confirms ductility without cracking
- Cast/helix check: spool wire only
- Certificate: EN 10204 3.1; 3.2 with TPI
Medical wire may also need ASTM F67 / F136; aerospace wire may need AMS 4951 / AMS 4954. B863 alone does not make wire “implant grade” or “aircraft grade”. [3,4](@ref)
8. How to Write an ASTM B863 / ERTi RFQ
Weak: "Titanium welding wire 1.6 mm"
Strong: ASTM B863 Gr.2 titanium wire, ERTi-2 per AWS A5.16, Ø1.6 mm, bright annealed, spool 5 kg, low-H, 100% ET, square-cut sample rejected, EN 10204 3.1, heat no. on spool label
Must specify:
- Product standard: ASTM B863 or ASME SB-863
- Filler class if welding: ERTi-1 / 2 / 5 / 9 / 12 / 23
- Grade: Gr.1 / Gr.2 / Gr.5 / Gr.9 / Gr.12 / Gr.23
- Diameter & tolerance: Ø1.6 mm, ±0.013 mm class
- Form: spool / coil / straight rod
- Condition: annealed / cold-worked / bright annealed
- Surface: pickled / bright / polished
- Package: 5 kg / 10 kg spool, 914 mm rods
- NDE: ET / UT / none
- Certificate: 3.1 / 3.2
9. Wire Procurement Mistakes That Ruin Welds
| Mistake | Result | Fix |
|---|---|---|
| “B863 Gr.2” on a welding PO, no ERTi class | QC argues whether it’s filler metal | Add “ERTi-2 per AWS A5.16” |
| Buying as-drawn wire for TIG | Porosity, contamination, arc instability | Use pickled or bright-annealed filler |
| Ignoring cast/helix on spool wire | Bird-nesting, feeding jams | Agree cast/helix in RFQ |
| ERTi-2 on Gr.5 base metal | Under-matched weld strength | Use ERTi-5 / ERTi-23 per WPS |
| No heat/lot label on spool | Traceability lost after opening package | Require heat no. + lot no. on every spool |
10. Our Wire, Filler & Welding Support
- ASTM B863 / SB-863 Gr.1, Gr.2, Gr.5, Gr.7, Gr.9, Gr.12, Gr.23
- AWS A5.16 ERTi-1 / 2 / 5 / 7 / 9 / 12 / 23
- Ø0.1–8.0 mm; spool 5/10 kg, coil, 500/914/1000 mm straight rods
- Pickled, bright-annealed, polished; low-hydrogen control
- 100% surface ET on fine/spool wire where specified
- WPS/PQR support for titanium pipe & vessel welding
- Compatible with B861/B862 pipe, B338 tube, B381 flange spools
- Laser label: grade + ERTi class + heat no. + lot no.
- EN 10204 3.1 / 3.2, AMS 4951 / 4954 on request
We supply weld-ready titanium filler, not mystery spools.
11. FAQs
Q: Is ASTM B863 wire the same as welding wire?
Not automatically. B863 defines the wire product; AWS A5.16 defines the welding-filler classification. For TIG/MIG, ask for the ERTi class explicitly. [7](@ref)
Q: What size is most common for titanium TIG welding?
1.6 mm and 2.4 mm straight rods or spool wire are very common for GTAW on pipe and exchangers.
Q: Can I use ERTi-2 to weld Gr.5 Ti-6Al-4V?
You can physically weld it, but the weld metal will be much weaker than the base metal. Use ERTi-5 or ERTi-23 per the qualified WPS.
Q: Does titanium wire need dry storage?
Yes. Store in low-humidity conditions, keep spools sealed until use, and never touch the wire with bare carbon-steel tools — iron contamination is the enemy.
Q: Can B863 wire be used for 3D printing / WAAM?
Yes. Fine spool wire in Gr.5 / Gr.23 is used as feedstock for wire arc additive manufacturing and DED, provided chemistry, diameter, and surface cleanliness match the machine spec. [3](@ref)
12. Related Standards
Request ASTM B863 Titanium Wire / Filler Quote
Send us:
- Grade + ERTi class (e.g., Gr.2 / ERTi-2)
- Diameter & tolerance
- Form: spool / coil / straight rod
- Surface: pickled / bright / polished
- Package weight & spool type
- NDE & certificate (3.1 / 3.2)
We reply within 4 business hours with grade cross-check, spool options, and lead time.
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
- Titanium pipe knowledge·tee + reducer selection 5 steps
- TA series vs TC series comparison: pure titanium vs titanium alloy s
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China