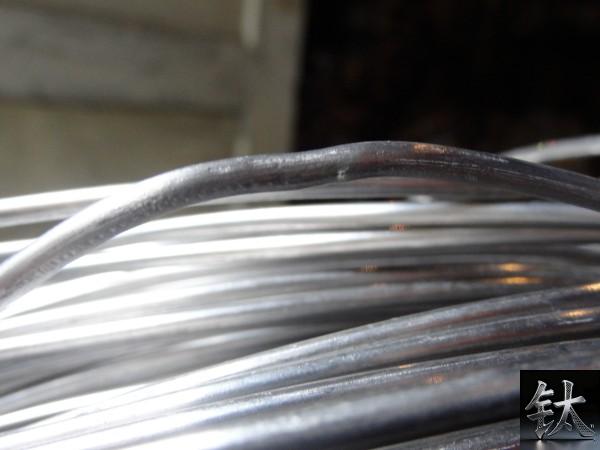
Titanium Welding Wire AWS A5.16 Supplier \| ERTi-1/2/5/7/23 Spool & TIG Rod, EN 10204 3.1, Baoji Stock
| Спецификация | titanium welding wire AWS A5.16 supplier, ERTi-1 ERTi-2 ERTi-5 AWS A5.16, titanium TIG rod spool Baoji, AWS A5.16 vs ASTM B863 titanium wire, EN 10204 3.1 titanium weld wire, ERTi-7 palladium wire, ER |
|---|---|
| Справочная цена | $30.00 – $50.00 |
Описание продукции: AWS A5.16 titanium welding wire supplier in Baoji — ERTi-1/2/5/7/23, TIG straight rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 with measured interstitials. Classification + revision + lo
Обзор продукции
Titanium Welding Wire AWS A5.16 Supplier | ERTi-1 / ERTi-2 / ERTi-5 / ERTi-7 / ERTi-23, TIG & MIG, MTC 3.1
Meta Description: AWS A5.16 titanium welding wire supplier in Baoji — ERTi-1/2/5/7/23, TIG straight rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 with measured interstitials. Classification + revision + lot on every spool. Lot confirmed before PI.
Overview — AWS A5.16 Is the Identity, Not a Buzzword
AWS A5.16 is the filler-metal spec for titanium arc welding (GTAW/GMAW/PAW). It does three things a "Gr1 wire" label cannot:
- Fixes the ERTi-X classification (filler, not base wire)
- Caps interstitials (O/N/H/C) by class — the real driver of weld ductility
- Requires identification: AWS class + manufacturer + size + lot/heat on every spool/rod unit
ASTM B863 is for non-welding wire (springs, fasteners, mesh). Same metal, different job. A code weld citing AWS A5.16 / D1.9 cannot be released on a B863 cert alone — the filler classification must be named. We supply both, but the PO decides which cert line ships.
ERTi Class Quick Selector
| AWS Class | Base equiv. | O max (band) | H max | Use |
|---|---|---|---|---|
| ERTi-1 | Gr1 | 0.10% | 0.005% (rod) | Max ductility, thin-wall chemical/sea, clad interlayer |
| ERTi-2 | Gr2 | 0.16% | 0.008% | Industrial workhorse, pressure vessel TIG/MIG |
| ERTi-4 | Gr4 | 0.32% | 0.008% | Higher-strength CP joints (less common) |
| ERTi-5 | Gr5 (TC4) | 0.20% | 0.015% | Ti-6Al-4V base, high-strength airframe/structure |
| ERTi-7 | Gr7 | 0.16% | 0.008% | Reducing/crevice-corrosion service (0.12–0.25% Pd) |
| ERTi-9 | Gr9 | 0.16% | 0.008% | Ti-3Al-2.5V tubing welds |
| ERTi-12 | Gr12 | 0.20% | 0.008% | Mo-Ni alloyed, hot brine service |
| ERTi-23 | Gr23 ELI | 0.11% | 0.005% | Fracture-critical / medical-adjacent |
Full chemistry bands per AWS A5.16 (rev stated on PO). MTC lists measured O/H/N/C — not "complies".
Forms & Sizes (AWS A5.16 Route)
| Form | Diameter | Package |
|---|---|---|
| TIG straight rod | 1.0 / 1.6 / 2.0 / 2.4 / 3.2 mm | 914 / 1000 mm, 5kg tube, flag-tagged |
| MIG spool | 0.8 / 1.0 / 1.2 / 1.6 mm | D200 (5kg) / D300 (10kg) vacuum-sealed |
| Coil (auto feed) | 0.6–2.0 mm | Moisture-barrier coil, PO-stated weight |
Custom wind to feeder model on request — tell us push / pull / dual, we layer-wind to match.
Why Interstitials Decide the Weld
- Oxygen: raises strength, kills ductility. Blue/grey bead = pickup, not cosmetic.
- Hydrogen: delayed cracking risk; vacuum anneal + sealed pack matter.
- Nitrogen: nitride skin, hard/brittle — purge must hold to cool.
- Carbon: carbide stringers hurt fatigue.
AWS A5.16 exists largely to police these four. Wire surface must be pickled/bright, oil-free, no drawing lube — argon-clean on arrival, kept sealed until the feeder.
Mechanical Reference (Deposit / Base Min.)
| Class | UTS min | YS min | Elong |
|---|---|---|---|
| ERTi-1 | 240 MPa | ~170 MPa | ≥24% |
| ERTi-2 | 345 MPa | 275 MPa | ≥20% |
| ERTi-5 | 895 MPa | 828 MPa | ≥10% |
| ERTi-23 | 860 MPa | 790 MPa | ≥10% |
Final joint properties = wire lot + your WPS/PQR + purge discipline. Wire alone doesn't make the weld pass.
Identification & Traceability (AWS A5.16 + EN 10204 3.1)
- Every spool/rod unit tagged: AWS class + manufacturer ID + Ø + lot/heat No.
- EN 10204 3.1, mill-authorized IR: measured chemistry (interstitials called out) + tensile + lot-to-ingot
- Sealed cert pouch: MTC + (UT/cleanliness report per PO)
- 3.2 (SGS/BV/TÜV) witness PO-fronted, not back-signed
- ERTi (filler) and B863 (base wire) never mixed on one cert line
Packaging Non-Negotiables
- Vacuum foil + desiccant + aluminium barrier
- D200/D300 plastic spool, no steel contact
- TIG rods: PE/kraft tube, ends capped, flag tag per rod
- Outer: plywood case / antistatic carton, "DRY / NO OIL / ARGON-CLEAN"
- Pre-ship photo: spool face + lot tag + seal
WPS Compliance — What We Confirm Before PI
- AWS A5.16 revision (latest cited on PO)
- ERTi class matched to base metal + WPS
- Ø + process (TIG/MIG/PAW) + spool type
- Interstitial ceiling (O/H/N) if tighter than class default
- Shielding note (Ar purity, back purge) — printer-side, but we align pack to it
- Cert type (3.1 default / 3.2 TPI named)
No "A5.16-compatible" vague stamp. Either the PO names the class, or we qualify it with you before dispatch.
Stock Scope (Honest)
| Class | Status |
|---|---|
| ERTi-1 / ERTi-2 | Core rotating (1.2/1.6/2.0/2.4mm) |
| ERTi-5 (TC4) | Annealed lot rotating; STA not pre-shipped |
| ERTi-7 / ERTi-9 / ERTi-12 | Project heats, PO-fronted |
| ERTi-23 ELI | Separate PO, F136/ISO 5832-3 chain |
No "all classes same-day". Lot confirmed → PI date = dispatch commitment.
Enquiry Template (Copy-Paste)
AWS A5.16 rev: ___ (e.g. A5.16/A5.16M)
Class: ERTi-1 / 2 / 5 / 7 / 23 ___
Diameter: ___ mm
Form: TIG straight (914/1000mm) / MIG spool D200/D300 / coil ___
Weight: 5kg / 10kg / ___ kg
Base metal: Gr1/2/5/7/9/12/23 ___
WPS attached? Y/N
Shielding: Ar ___% / back purge Y/N
Interstitial cap: O___% H___ppm
Cert: 3.1 / 3.2 (TPI: ___)
Qty: ___ spools / ___ tubes
Incoterm: EXW Baoji / FOB Shanghai / DAP ___
FAQ — AWS A5.16 Titanium Welding Wire
Q1: AWS A5.16 vs ASTM B863 — which cert do I need?
A: Welding filler → AWS A5.16 (ERTi class). Springs/fasteners/mesh → ASTM B863. Code welds cite A5.16; B863 alone won't clear QA on a WPS.
Q2: Can ERTi-2 weld Gr5 base?
A: Feedable, ductile, but understrength vs Gr5. Match ERTi-5 unless the welding engineer approves undermatching in the WPS.
Q3: Is "Gr5 wire" the same as ERTi-5?
A: Not on paper. ERTi-5 is the A5.16 filler classification with interstitial bands. PO must say ERTi-5 + revision.
Q4: Blue bead — wire fault?
A: Usually purge/contamination, not chemistry. Wire ships argon-clean; chamber/argon dewpoint is printer-side.
Q5: MTC real numbers?
A: Yes — measured O/H/N/C/Fe + tensile + lot. Not minima-only.
Q6: STA ERTi-5 from shelf?
A: No. Annealed default. STA = PO-stated heat treat + re-MTC.
Q7: Medical implant weld?
A: ERTi-23 ELI + F136/ISO 5832-3 chain, separate PO, clean-pack. Industrial ERTi-5 ≠ implant.
Q8: Spool tangle?
A: Precision layer-wind to feeder type. State push/pull/dual at enquiry.
Q9: Custom diameter / D300+?
A: PO-fronted, melt schedule quoted before PI. Core sizes move same-week after lot confirm.
Q10: Quote time?
A: 24h with class + Ø + form + qty + incoterm. Lot status confirmed before PI.
Request a Quote
Email: sales@[yourdomain].com
Send AWS class + revision + Ø + form + WPS note. Reply in 24h: lot No., EXW/FOB price, cert type, dispatch date.
About: Baoji Titanium Valley AWS A5.16 welding-wire supplier. ERTi-1/2/5/7/9/12/23 — TIG rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 with measured interstitials. Classification + revision + lot on every unit. We don't stamp "A5.16" on a B863 cert. Name the WPS, get the right ERTi class, sealed clean, dispatched on the PI date.
Опишите ваши требования — марка, размер и количество. Ответим в течение 24 часов.
Предпочитаете чат? WhatsApp +86 188 2967 9311 или напишите на sales@sxqytd.com.
- Titanium Price Today (26 октября 2026 г.): отчет о рынке Китая
- Цена на титан сегодня (23 октября 2026 г.): пластина, трубка, стерже
- Читайте титановую проволоку и проволоку из титанового сплава: класси
- Титановая проволока: от выбора марки до производственного процесса (
- Читайте титановую трубку и трубку из титанового сплава: классификаци
Контактное лицо: Wang Xiaoning
Телефон: +86-917-355-7966
Эл. почта: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Компания: Shaanxi Qianyi Tuoda Technology Co., Ltd
Адрес: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China