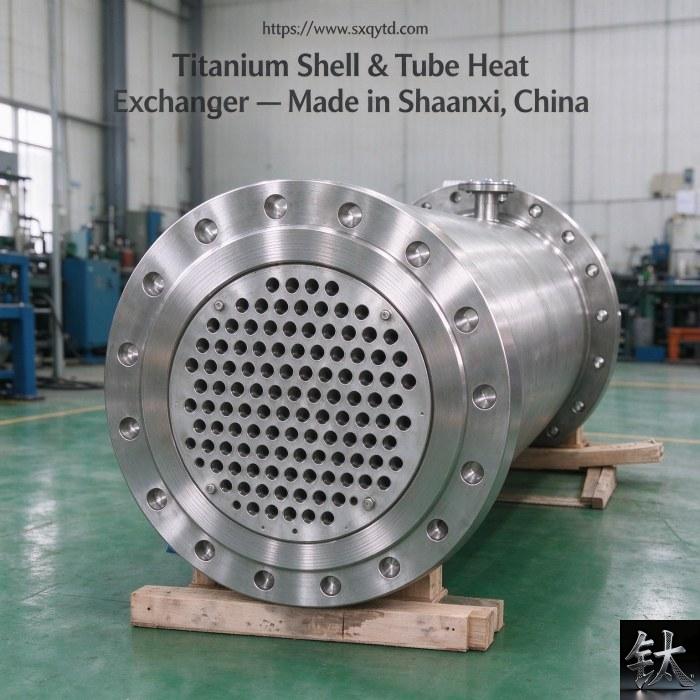
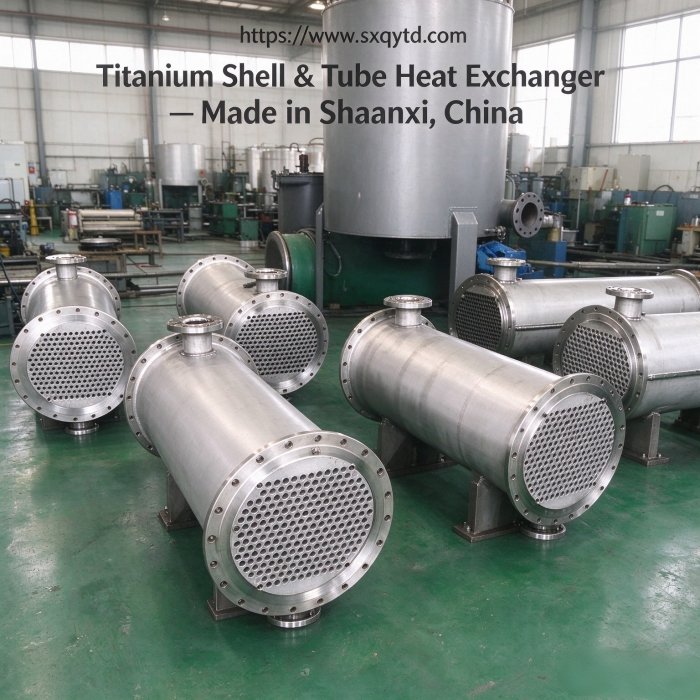
Titanium Heat Exchanger with EN 10204 3.1 MTC
| Спецификация | ASTM B338/B265, Heat-Number Traceable, PMI, ASME VIII + TEMA, Baoji |
|---|---|
| Применимый стандарт | This titanium heat exchanger is supplied with EN 10204 3.1 material test certificate. Each batch of titanium raw tube, sheet and forging is traceable with full mill documentation before fabrication. |
| Состояние материала | All welding joints go through hydrostatic pressure test and helium leak detection. Inspection records are cross-checked to match the data shown on the 3.1 MTC. 2. We can submit certificate documents |
Описание продукции: Titanium shell-and-tube heat exchanger supplied with EN 10204 Type 3.1 MTC — ASTM B338 tube / B265 tubesheet, heat-number traceable from melt to tube tag to weld map, PMI per heat, eddy-current/hydro
Обзор продукции
Titanium Heat Exchanger with EN 10204 3.1 MTC | Heat-Number Traceable, ASTM B338/B265, ASME VIII + TEMA
Meta Description: Titanium shell-and-tube heat exchanger supplied with EN 10204 Type 3.1 MTC — ASTM B338 tube / B265 tubesheet, heat-number traceable from melt to tube tag to weld map, PMI per heat, eddy-current/hydro per B338 election, non-chlorinated PT on seal welds. 3.1 = material conformance; ASME VIII = fabrication; 3.2 TPI PO-fronted where required.
What EN 10204 3.1 Actually Certifies
A Type 3.1 MTC is not a generic "quality certificate". It is a heat-specific, inspection-specific test report issued by the manufacturer's independent inspection function (separate from production). For a titanium exchanger it must show:
- Grade + UNS (R50400 / R52400 / R56320 / R53400…)
- Standard: ASTM B338 (tube) / B265 (tubesheet/plate)
- Heat number — matching tube tag, bundle label, packing list
- Actual chemistry: Ti balance, O/N/H/C/Fe, plus Pd for Gr7, Mo-Ni for Gr12
- Mechanical results: tensile, yield, elongation (annealed values)
- Test method/election: ET or hydro per B338, flatten/flare or reverse-flatten
- Delivery condition: annealed, pickled/bright, dimensions/tolerances
- Independent QA signature (not the rolling operator)
3.1 proves the material supplied matches the grade on the PO. It does not, by itself, certify the weld or the ASME calculation — those are covered by the MDR and U-1A.
3.1 vs 3.2 vs ASME U-Stamp (stop confusing them)
| Document | What it covers | Who signs | When needed |
|---|---|---|---|
| EN 10204 3.1 | Material conformance per heat (chemistry + mech + NDT election) | Mill/manufacturer independent QA | Default for chemical/desalination/marine EPC |
| EN 10204 3.2 | 3.1 content + purchaser/third-party (SGS/BV/TÜV) countersign | QA + TPI witness | Critical/safety-class items, PO-named TPI |
| ASME VIII U-1A | Design calc, fabrication, pressure test, weld map | Authorized Inspector (AI) | ASME-coded pressure equipment |
Rule: 3.2 cannot be issued after fabrication — TPI must be named at PO stage. Asking for "3.2 later" is not a workflow.
Heat-Number Chain (the only real traceability)
Traceability is not a logo on the cert. It is a closed loop:
Melter heat record
   → Billet/flat product heat
   → Tube MTC (3.1) heat No.
   → Tube body stamp / laser tag
   → Bundle label + packing list
   → Weld map (tube heat × tubesheet heat)
   → As-built MDR dossier
Cut-to-length pieces carry the parent heat via transferred marking or controlled cut records — never a fresh "Gr2" sticker with no heat reference.
Gr7 Special Clause — Pd Must Be on the 3.1
- Gr7 = R52400, Pd 0.12–0.25% — if the 3.1 omits Pd, it does not prove Gr7
- Arrival PMI (OES/XRF) verifies Pd in the matrix; PMI supports, does not replace, full chemistry
- Weld filler ERTi-7 to keep HAZ corrosion performance consistent
- "Grade 7" printed on a tag without Pd chemistry = incomplete certification
Inspection Stack Delivered With the Unit
- ASTM B338 tube MTC EN 10204 3.1 (heat-specific)
- ASTM B265 tubesheet MTC 3.1 (solid or clad overlay)
- Eddy-current or hydrostatic per B338 election (stated on PO)
- PMI report per heat (XRF/OES)
- PT on U-bends + tube-to-tubesheet seal welds (non-chlorinated penetrant)
- Weld map + WPS/PQR (ASME IX)
- ASME VIII calc package + TEMA data sheet + U-1A (coded units)
- Hydro test record; helium leak option for critical duty
- 3.2 TPI witness record when PO-fronted (SGS/BV/TÜV/DNV)
What 3.1 Does NOT Do (no overclaim)
- Does not choose the grade for your process — PO must state service chemistry
- Does not certify the weld — that is WPS/PQR + PT/leak test + AI review
- Does not equal ASME stamp — separate document chain
- Does not retroactively become 3.2 — TPI must witness before/during production
- Does not cover HF/fluoride service — titanium excluded, separate alloy review
Procurement Red Flags (reject quietly, before PO)
- MTC says "Grade 2" but no heat number → reject
- Heat number on tube ≠ heat number on cert → stop
- Gr7 cert without Pd value → not provable Gr7
- Only PDF cert, no weld map, no PMI → audit will fail
- "3.2 available after shipment" → not how EN 10204 works
- Chlorinated PT penetrant on titanium → crevice risk planted at QA stage
RFQ / Doc-Requirement Template (copy-paste)
Tube: ASTM B338 Gr___, OD×wall ___, heat-number tag required Y/N
Tubesheet: B265 Gr___, solid / clad (__mm Ti)
Cert: EN 10204 3.1 (default) / 3.2 TPI (SGS/BV/TÜV ___, named at PO)
MTC fields required: heat No., Pd (Gr7), O/N/H/C/Fe, tensile, ET/hydro election
PMI: per heat, XRF/OES, report attached Y/N
Cut pieces: transferred heat marking / cut-record map ___
NDE: ET ___ / hydro ___ / PT(non-Cl) ___ / helium (__ mbar·L/s)
Code docs: ASME VIII calc + TEMA sheet + U-1A + weld map ___
Packaging: seaworthy, Ti segregated from CS, cert in waterproof pocket ___
FAQ — Titanium Exchanger + EN 10204 3.1
Q1: Is 3.1 enough for EPC desalination/chemical projects?
A: Yes — 3.1 with heat-number closure + PMI is the standard acceptance baseline. 3.2 is added only when the owner/PO mandates TPI witness.
Q2: Can cut-to-length tubes keep 3.1 traceability?
A: Yes, via transferred marking or controlled cut records linking sub-pieces to the parent heat. No heat number = no real 3.1.
Q3: Does 3.1 prove the exchanger is ASME-compliant?
A: No. 3.1 proves material; ASME VIII/U-1A proves design+fabrication. Both ships in the MDR, but they are different documents.
Q4: How do I verify Gr7 from Gr2 by paper?
A: Pd 0.12–0.25% on the 3.1 chemistry line + PMI on arrival. No Pd line = not a verifiable Gr7 cert.
Q5: PMI or 3.1 — which is stronger?
A: 3.1 is the primary conformance record (lab chemistry). PMI is field verification. Use both; PMI does not replace lab analysis for low-level Pd.
Q6: Can you issue 3.2 after fabrication?
A: No. EN 10204 3.2 requires TPI involvement during the inspection window. Name the TPI at PO; witness points are planned, not backdated.
Q7: What about welded vs seamless tube certification?
A: Both carry B338 + 3.1. Welded tube adds reverse-flatten/seam NDE; election stated on PO, not assumed.
Q8: Packaging for export?
A: Ti segregated from carbon steel, ferroxyl-free surface, cert in waterproof pocket, ISPM-15 timber, heat/lot cross-linked to packing list.
Q9: Biggest audit failure mode?
A: Cert looks fine, but heat number on tube tag ≠ heat number on MTC. Closed-loop traceability is what auditors actually check.
Request a Document-Compliant Quote
Email: sales@[yourdomain].com
Send tube spec + service chemistry + cert level (3.1 / 3.2 TPI) + code level. We return a document scope list with the quote — not certs "to follow later".
About: Baoji titanium exchanger documentation desk — ASTM B338 tube / B265 tubesheet shell-and-tube units and replacement bundles with EN 10204 Type 3.1 MTC as default. Heat number closed from melt → tube tag → weld map → as-built MDR. PMI per heat, non-chlorinated PT, roll+seal-weld joints, ASME VIII + TEMA. Gr7 MTC declares Pd 0.12–0.25%; 3.2 TPI PO-fronted, never back-issued. Certificate chain delivered with the unit, not negotiated after.
Опишите ваши требования — марка, размер и количество. Ответим в течение 24 часов.
Предпочитаете чат? WhatsApp +86 188 2967 9311 или напишите на sales@sxqytd.com.


- Titanium Price Today (26 октября 2026 г.): отчет о рынке Китая
- Цена на титан сегодня (23 октября 2026 г.): пластина, трубка, стерже
- Читайте титановую проволоку и проволоку из титанового сплава: класси
- Титановая проволока: от выбора марки до производственного процесса (
- Читайте титановую трубку и трубку из титанового сплава: классификаци
Контактное лицо: Wang Xiaoning
Телефон: +86-917-355-7966
Эл. почта: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Компания: Shaanxi Qianyi Tuoda Technology Co., Ltd
Адрес: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China