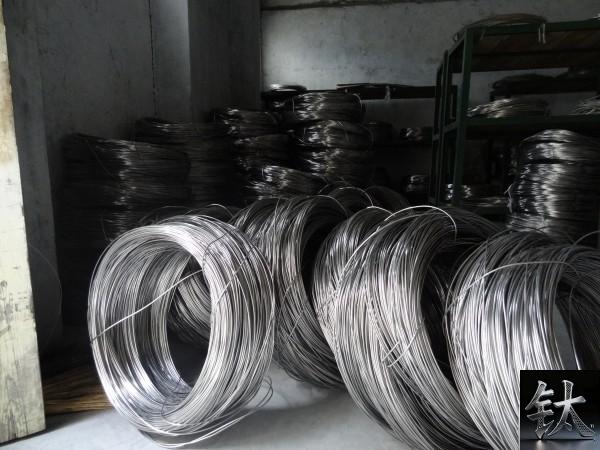
Gr1 Titanium Wire for Welding Stock \| ERTi-1 AWS A5.16 / ASTM B863, Spool & TIG Rod, MTC 3.1, Baoji Stock
| Specification | Gr1 titanium welding wire stock, ERTi-1 titanium wire AWS A5.16, ASTM B863 Gr1 wire, titanium TIG rod 1.6 2.4 3.2mm, MIG spool ERTi-1 Baoji, CP titanium filler wire seawater chemical, titanium weld wi |
|---|---|
| Reference Price | $20.00 – $30.00 |
Product Description: Gr1 / ERTi-1 titanium welding wire in stock from Baoji — AWS A5.16 / ASTM B863, Ø0.8–3.2mm TIG & MIG, spool/coil/straight rod, bright pickled, EN 10204 3.1 heat/lot traceable. For chemical/sea/explosi
Product Overview
Gr1 Titanium Wire for Welding Stock | ERTi-1 (AWS A5.16) & ASTM B863, TIG/MIG, MTC 3.1
Meta Description: Gr1 / ERTi-1 titanium welding wire in stock from Baoji — AWS A5.16 / ASTM B863, Ø0.8–3.2mm TIG & MIG, spool/coil/straight rod, bright pickled, EN 10204 3.1 heat/lot traceable. For chemical/sea/explosive-cladding welds. Quote with WPS + diameter + package.
Overview — Welding Wire Is a Consumable, Not a Bar
The first mistake in titanium weld-wire procurement: writing "Gr1 wire" and expecting it to clear QA. There are two correct descriptions:
- Base-material wire → ASTM B863 Gr1 (structural/forming wire)
- Welding filler (correct for GTAW/GMAW) → ERTi-1 per AWS A5.16 / ISO 24034
ERTi-1 caps interstitials tighter (O ≤0.10% per AWS A5.16 filler class) than generic B863 Gr1 base stock. We stock both, but the PO must name the spec. A weld inspected to a WPS citing ERTi-1 cannot be released on a "Gr1 B863" cert alone — classification and revision decide acceptance.
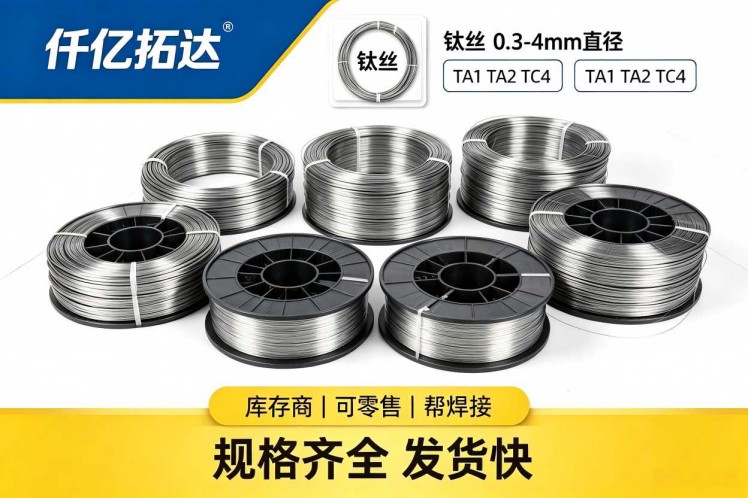
Baoji Titanium Valley stock: ERTi-1 spools for MIG, straight TIG rods for GTAW/PAW, bright-pickled, argon-clean, lot-traceable. Annealed, low-interstitial, heat No. on every spool.
Why Gr1 / ERTi-1 for Welding
- Softest CP titanium — highest ductility, lowest crack sensitivity in the weld metal
- Best for thin-wall chemical pipe, heat-exchanger tube-to-tubesheet, seawater liner repair
- Matching filler for Gr1 base; undermatching (softer) filler for Gr2/Gr3 where ductility > strength
- Explosive cladding interlayer (Ti-steel transition) — absorbs impact, prevents interface cracking
- Ultra-clean weld pool with proper argon purge — no post-weld brittlement from interstitials
Rule of thumb: if the joint is corrosion-driven, not strength-driven → ERTi-1. If design stress needs Gr2/Gr5 strength → match the filler to the base + WPS, don't "upgrade" to Gr1 blindly.
Stock Scope (Honest)
| Form | Diameter | Package | Spec | Status |
|---|---|---|---|---|
| TIG straight rod | 1.0 / 1.6 / 2.0 / 2.4 / 3.2 mm | 914mm / 1000mm straight, 5kg tube | ERTi-1 AWS A5.16 | Rotating stock |
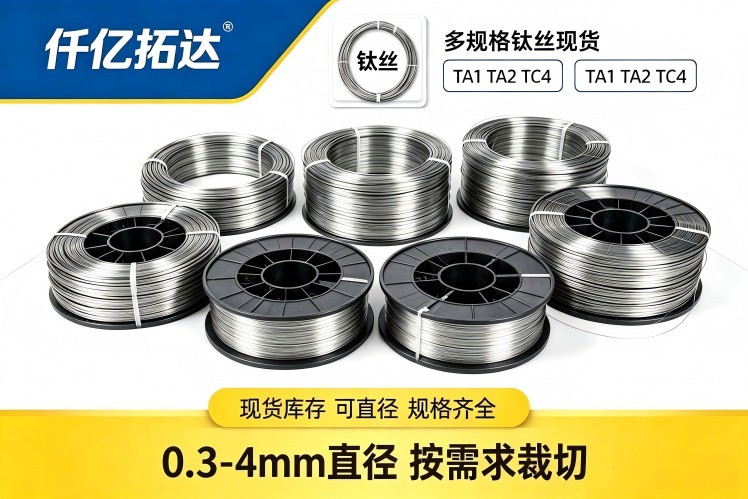
| MIG spool | 0.8 / 0.9 / 1.0 / 1.2 / 1.6 mm | D200/D300 spool, 5kg/10kg vacuum-sealed | ERTi-1 AWS A5.16 | Core sizes on hand |
| Coil (auto feed) | 0.6–2.0 mm | Coil + moisture barrier | ERTi-1 / B863 Gr1 | Per PO |
| Base wire (non-consumable) | Ø0.1–6.0 mm | Coil/spool/straight | ASTM B863 Gr1 / F67 (industrial) | Project stock |
Honest line: common TIG diameters (1.6/2.4/3.2mm) and 1.2mm MIG move fast. Custom spool weight / D300+ / F67 medical chain = PO-fronted, not ghost shelf.
Chemistry — ERTi-1 Filler vs B863 Gr1 Base
| Element max | ERTi-1 (AWS A5.16) | Gr1 base (ASTM B863 ref.) |
|---|---|---|
| O | 0.10% | 0.18% |
| Fe | 0.20% | 0.20% |
| N | 0.03% | 0.03% |
| C | 0.03% (filler class) | 0.08% |
| H | 0.005% (rod) / 0.008% (electrode) | 0.015% |
| Ti | Balance (99.5%+) | Balance |
The gap is oxygen + hydrogen. That is why "Gr1-ish" base wire is not a drop-in for ERTi-1 in a code weld.
Mechanical Reference (Annealed)
| Item | Value |
|---|---|
| UTS (Gr1 base / deposit min) | ≥240 MPa (AWS A5.16 deposit min) |
| YS | ~170 MPa (typical) |
| Elongation | ≥24% |
| Density | 4.51 g/cm³ |
MTC carries measured chemistry + tensile per lot. Weld strength is governed by WPS/PQR, not by the rod brochure number.
Welding Reality — What Makes ERTi-1 Weld Clean
- Shielding: 99.995% Ar min; DCEN for TIG, DCEP for MIG
- Back purge mandatory until weld cools below ~427°C (800°F)
- Trailing shield recommended for open-position titanium joints
- Wire surface: pickled/bright, no oil, no drawing lube residue
- Color check: straw/blue = interstitial pickup; silver = clean. Blue bead is a rejection signal, not a cosmetic issue
- Store sealed; open only at the feeder. Moisture + dust = porosity
Diameter / Process Quick Map
| Process | Common Ø | Use |
|---|---|---|
| GTAW (TIG) | 1.0 / 1.6 / 2.4 / 3.2 mm straight | Tube-sheet, thin-wall pipe, field repair |
| GMAW (MIG) | 0.8 / 1.0 / 1.2 mm spool | Auto weld, long seams, tank fabrication |
| PAW | 0.8–1.6 mm | Precision thin-gauge |
| Explosive clad interlayer | 1.5–2.0 mm coil | Ti-steel composite plate |
Traceability & Inspection
- EN 10204 3.1, mill-authorized IR — chemistry (interstitials called out) + tensile + lot No.
- Spool/bundle tag: AWS class + diameter + lot/heat + manufacturer ID
- PMI / surface cleanliness check on PO
- 3.2 (SGS/BV/TÜV) witness PO-fronted, not back-signed
- Lot-to-ingot traceability; no relabel of B863 base as ERTi-1 without filler-class cert
Packaging for Weld Wire (Non-Negotiable)
- Vacuum-sealed pouch / aluminium foil + desiccant
- D200/D300 plastic spool, no steel contact
- TIG rods in sealed kraft + PE tube, ends capped
- Outer: plywood case / carton, "DRY / NO OIL / ARGON-CLEAN" label
- Pre-ship photo: spool face + lot tag + seal integrity
Enquiry Template (Copy-Paste for Welding Buyers)
Filler class: ERTi-1 (AWS A5.16 rev ___) / ASTM B863 Gr1 ___
Process: GTAW / GMAW / PAW ___
Diameter: ___ mm
Package: straight 914/1000mm / D200 / D300 / coil ___
Weight: 5kg / 10kg / per coil ___
Base metal: Gr1 / Gr2 / clad / other ___
WPS/PQR: attached? Y/N   (or WPS class required ___)
Shielding: Ar purity ___%, back purge Y/N
Surface: bright pickled / as-drawn cleaned
Cert: 3.1 / 3.2 (TPI: ___)
Qty: ___ spools / ___ kg
Incoterm: EXW Baoji / FOB Shanghai / DAP ___
FAQ — Gr1 / ERTi-1 Welding Wire Stock
Q1: Is "Gr1 wire" the same as ERTi-1?
A: No. B863 Gr1 = base/material wire; ERTi-1 = AWS A5.16 filler classification with tighter O/H ceilings. Code welds cite ERTi-1 — PO must say so.
Q2: Which diameter for TIG pipe repair?
A: 1.6mm thin wall; 2.4mm general; 3.2mm heavier section. Match to amperage + joint prep, not "thicker is safer".
Q3: Can ERTi-1 weld Gr2 base?
A: Yes — undermatching filler (softer deposit). Acceptable where WPS allows; strength governed by PQR, not rod grade alone.
Q4: Why blue weld bead = problem?
A: Color = oxygen/nitrogen pickup. Silver/straw = clean; blue/purple = interstitial contamination, re-check purge + wire cleanliness.
Q5: MTC real interstitials?
A: Yes — 3.1 lists O/N/H/C/Fe measured, not just "complies". That is what WPS auditors want.
Q6: Spool or straight rod?
A: MIG/auto = spool; field TIG = straight 914/1000mm. Don't run straight rod through a MIG feeder.
Q7: Medical F67 wire?
A: Industrial Gr1/B863 ≠ implant F67 chain. Medical path = separate PO, F67/F136 docs, clean-room pack.
Q8: Explosive cladding use?
A: ERTi-1 1.5–2.0mm coil is standard interlayer — ductility absorbs clad shock, prevents delamination.
Q9: Dispatch?
A: Common TIG/MIG sizes same-week after PO + lot confirm. Custom spool/D300+/F67 PO-fronted lead quoted honest.
Q10: Trial lot?
A: 1 spool / 5kg TIG tube from current lot, deductible from bulk PO — qualify the weld, not just the price.
Request a Quote
Email: sales@[yourdomain].com
Send AWS class + Ø + process + package + WPS note. Reply in 24h: lot No., EXW/FOB price, cert type, dispatch date.
About: Baoji Titanium Valley welding-consumable stockist. Gr1 / ERTi-1 titanium welding wire — AWS A5.16 / ASTM B863, TIG rod + MIG spool, bright-pickled, argon-clean, EN 10204 3.1 lot-traceable. We do not relabel base wire as filler. Name the WPS, get the right classification, sealed clean, dispatched on the PI date.
Tell us your requirement — grade, size and quantity. We reply within 24 hours.
Prefer chat? WhatsApp +86 188 2967 9311 or email sales@sxqytd.com.
- Titanium Price Today (Oct 26, 2026): China Market Report
- Titanium Price Today (23 Oct 2026): Plate, Tube, Rod & Wire
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China