ASTM B862 Titanium Welded Pipe: Large-Diameter & Cost Guide
ASTM B862 Titanium Welded Pipe: Large-Diameter, Cost-Effective Piping & Specification Guide

Table of Contents
- 1. What Is ASTM B862?
- 2. B862 Welded vs. B861 Seamless: When to Choose Which
- 3. Common B862 Grades
- 4. Size Range & Wall Thickness
- 5. How Titanium Welded Pipe Is Made
- 6. Mandatory Weld Testing: ET, UT, Hydrostatic
- 7. How to Write an ASTM B862 RFQ
- 8. Cost Comparison: Welded vs. Seamless
- 9. Common Mistakes in Specifying Welded Pipe
- 10. Our B862 Supply & Fabrication
- 11. FAQs
- 12. Related Standards
1. What Is ASTM B862?
ASTM B862 is the standard specification for titanium and titanium alloy welded pipe. It covers pipe formed from titanium strip or plate and fusion-welded, typically used for large-diameter, low-to-medium pressure fluid transport.
The ASME version is SB-862. While B861 (seamless) dominates smaller NPS and high-pressure lines, B862 is the go-to for NPS 8" and above where the cost of seamless becomes prohibitive.
Bottom line: If your line is NPS 8" or larger, operating below 20 bar, and not in a fatigue-critical path — B862 welded pipe should be on your drawing.
2. B862 Welded vs. B861 Seamless: When to Choose Which
| Factor | B862 Welded | B861 Seamless |
|---|---|---|
| NPS range | NPS 4" to NPS 48"+ | NPS ½" to NPS 24" |
| Pressure class | Low to medium (typically < 40 bar) | Low to very high (up to 250+ bar) |
| Relative cost | Baseline (30–50% savings vs. seamless) | Premium |
| Weld seam | One longitudinal weld | None |
| NDT requirement | ET + UT + hydrostatic mandatory | UT or ET + optional hydrostatic |
| Lead time | Typically 3–6 weeks | 4–10 weeks (depending on size) |
| Best for | Seawater intake, outfall, cooling water, stack liners | Process headers, high-pressure chemical, offshore risers |
Many EPC firms now write dual-spec: "ASTM B861 or B862, per vendor proposal" — letting price drive the decision for non-critical lines.
3. Common B862 Grades
| Grade | Why specify | Typical B862 service |
|---|---|---|
| Gr.2 | Cost-effective, fully weldable, excellent corrosion | Seawater intake/outfall, cooling water mains, brine lines |
| Gr.7 | Pd-added, reducing-acid resistant | Chemical plant transfer lines, acid drain |
| Gr.12 | Hot chloride / crevice resistance | Geothermal brine, FGD scrubber piping |
| Gr.1 | Maximum ductility, easier forming of large diameters | Extra-large OD thin-wall pipe, stack liners |
Gr.2 is the default for 80%+ of B862 orders. The strip or plate used for forming must conform to ASTM B265, and the weld filler (if used) to B863 / AWS A5.16.
4. Size Range & Wall Thickness
- NPS range: 4" through 48"+ (OD 114 mm to 1220 mm+)
- Wall thickness: Sch 5S, 10S, custom from 2 mm to 25 mm+
- Lengths: single random (4–7 m), double random (7–14 m), or fixed
- Ovality: within ±1% of OD for most sizes
- Straightness: ≤ 3 mm per meter typical
Because B862 starts from flat strip/plate, ultra-large diameters and non-standard wall thicknesses are easier and cheaper than with seamless. Custom ODs like 520 mm, 760 mm, or 910 mm are routine.
5. How Titanium Welded Pipe Is Made
- Forming: Titanium strip/plate (B265 compliant) is rolled into a cylindrical shape.
- Tack welding: Ends are tack-welded under local argon shielding.
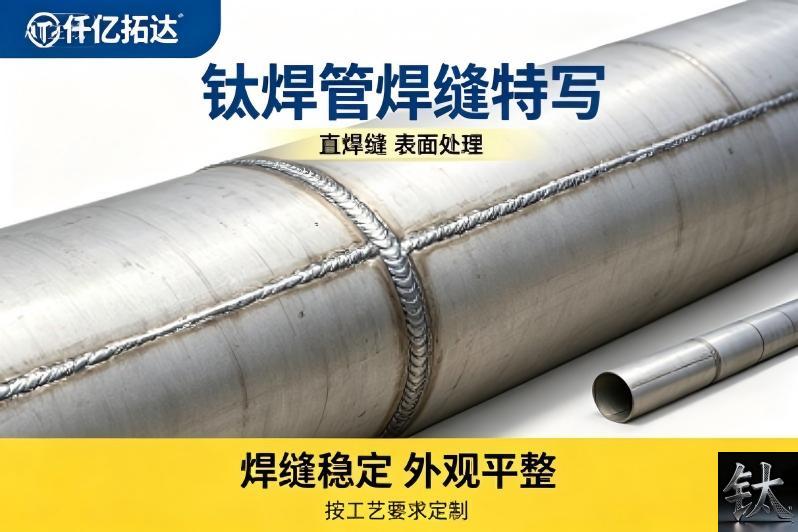
- Longitudinal welding: GTAW (TIG) or PAW (plasma arc) with trailing argon shield; automatic keyhole or melt-in mode.
- Weld trimming: Internal and external weld bead is trimmed flush.
- Post-weld annealing: Full-body heat treatment (typically 650–760°C) in inert atmosphere to restore ductility and relieve stress.
- Pickling / passivation: Removes α-case from heat-affected zone.
- Sizing & straightening: Cold sizing pass ensures roundness and straightness.
- Final NDT: ET, UT, hydrostatic per specification.
The weld is NOT the weak point — if the pipe fails, it almost always fails in the base metal, not the seam.
6. Mandatory Weld Testing: ET, UT, Hydrostatic
ASTM B862 requires all three for welded pipe (unlike seamless, where NDT is optional):
| Test | Standard | Purpose |
|---|---|---|
| Eddy Current (ET) | ASTM E426 | Detects surface and near-surface defects in weld seam |
| Ultrasonic (UT) | ASTM E213 | Detects internal discontinuities in weld and HAZ |
| Hydrostatic | ASTM B862 Section 8 | Verifies pressure integrity of finished pipe |
Additional tests on request:
- Flattening test (weld at 90° and 0°)
- Flange test on weld section
- Reverse-bend test on weld specimen
- Chemical analysis of base metal and weld deposit
- Ferrite count (if duplex filler used — rare in titanium)
- EN 10204 3.1 MTR (3.2 with third-party)
7. How to Write an ASTM B862 RFQ
Weak: "Welded titanium pipe 12 inch"
Strong: ASTM B862 / SB-862 Gr.2 welded pipe, NPS 12" Sch 10S, 6096 mm RL, BE ends, longitudinal weld GTAW, full-body anneal 700°C, 100% ET per ASTM E426 + UT per E213 + hydrostatic 15 bar, pickled, EN 10204 3.1
Must specify:
- Standard: ASTM B862 or ASME SB-862
- Grade: Gr.1 / Gr.2 / Gr.7 / Gr.12
- NPS & Schedule (or exact OD × WT)
- Length & quantity
- Ends: PE / BE
- Welding process: GTAW / PAW
- Post-weld heat treatment: yes / no / temperature
- NDT: ET + UT + hydrostatic (minimum)
- Surface finish: pickled / bright annealed
- Certificate: 3.1 / 3.2
8. Cost Comparison: Welded vs. Seamless
| NPS | B862 Welded (relative) | B861 Seamless (relative) | Savings |
|---|---|---|---|
| 4" Sch 10S | 1.0× | 1.4× | ~30% |
| 8" Sch 10S | 1.0× | 1.6× | ~35–40% |
| 12" Sch 10S | 1.0× | 1.8× | ~45% |
| 24" Sch 10S | 1.0× | 2.2× (if available) | ~50%+ |
Note: Ratios are indicative. Actual pricing depends on market, quantity, and mill allocation.
For large projects (seawater desalination, power plant cooling, FGD scrubbers), switching from B861 to B862 on non-critical lines can save $50,000–$500,000+ per project.
9. Common Mistakes in Specifying Welded Pipe
| Mistake | Consequence | Fix |
|---|---|---|
| Specifying seamless where welded is acceptable | Budget overrun, long lead time | Review P&ID with corrosion engineer; downgrade non-critical lines |
| No weld NDT specified | Uninspected seam ships | Write "100% ET + UT + hydrostatic per B862" |
| Forgetting post-weld anneal | Brittle HAZ, poor bendability | Specify full-body anneal 650–760°C |
| Using carbon-steel backing ring inside titanium weld | Iron contamination, crevice corrosion | Use titanium backing ring or open-root GTAW with argon purge |
| Not specifying pickling after weld | α-case remains on seam surface | Add "pickled and passivated after welding" |
10. Our B862 Supply & Fabrication
- ASTM B862 / SB-862 Gr.1, Gr.2, Gr.7, Gr.12
- NPS 4" through 48"+; custom ODs available
- GTAW / PAW longitudinal seam welding with full argon shielding
- 100% ET + UT + hydrostatic on every pipe
- Full-body annealing in inert atmosphere
- Pickled, passivated, VCI-wrapped, end-capped
- Spool prefabrication: pipe + flange + fitting pre-assembled and welded
- WPS/PQR and welder qualifications available
- EN 10204 3.1 / 3.2 certification
We don't just sell welded pipe — we deliver inspected, annealed, installation-ready titanium piping.
11. FAQs
Q: Is B862 welded pipe acceptable for ASME B31.3 service?
Yes. ASTM B862 is listed as an approved material standard in ASME B31.3, provided the pipe meets the NDT and pressure-test requirements of the standard.
Q: Can B862 pipe be used for vacuum service?
Yes, but specify seamless (B861) for high-vacuum or cyclically-loaded vacuum lines. For rough vacuum and constant-pressure vacuum transfer, B862 is acceptable.
Q: How long will a B862 Gr.2 seawater pipe last?
In normal seawater (≤ 40°C, clean, aerated), titanium Gr.2 shows zero measurable corrosion after 20–30 years. The weld seam is not a corrosion weak point.
Q: Can I get B862 pipe with a 3.2 certificate?
Yes. We can arrange TPI (third-party inspection) witness at the mill or our facility for hydrostatic, UT, ET, and dimensional checks.
Q: What's the largest diameter B862 pipe you can supply?
Standard production goes to NPS 48" (1219 mm OD). Larger diameters up to 2000 mm+ are available on project basis using custom plate rolling.
12. Related Standards
Request ASTM B862 Titanium Welded Pipe Quote
Send us:
- Grade & NPS (or exact OD × wall)
- Length & quantity
- End condition (PE / BE)
- Weld process preference (if any)
- NDT requirements (ET / UT / hydrostatic pressure)
- Certificate level (3.1 / 3.2)
We'll respond within 4 business hours with pricing, test plan, and lead time.
- Read titanium wire and titanium alloy wire: diameter classification
- Titanium wire: from brand selection to manufacturing process (2026 r
- Read titanium tube and titanium alloy tube: OD classification + comm
- Titanium pipe knowledge·tee + reducer selection 5 steps
- TA series vs TC series comparison: pure titanium vs titanium alloy s
Contact Person: Wang Xiaoning
Tel: +86-917-355-7966
Email: sales@sxqytd.com
WhatsApp: +86 188 2967 9311
Company: Shaanxi Qianyi Tuoda Technology Co., Ltd
Address: Floor 4, Building 4, No. 188 Gaoxin Avenue, High-tech Zone, Baoji City, Shaanxi Province, China